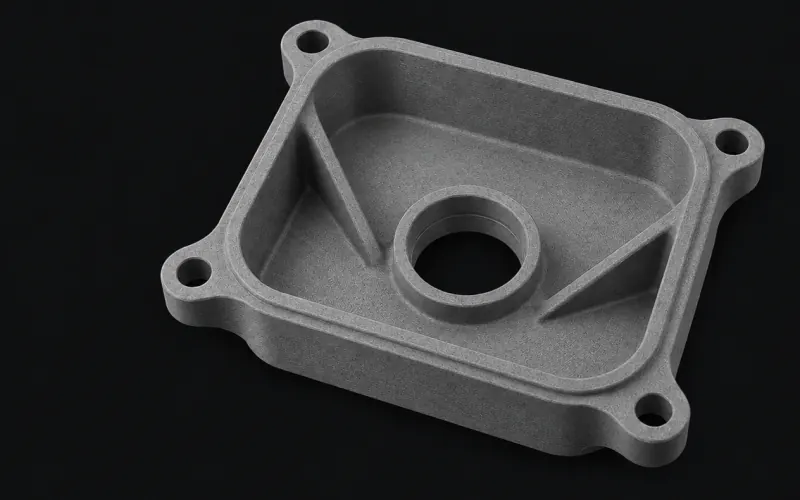
PA12 Nylon
Rigid and tough. Resists wear, oils, and greases.
- For
- Functional housings · Brackets · Ducts · Assembly fixtures
- Finish
- Natural gray · Black dyed


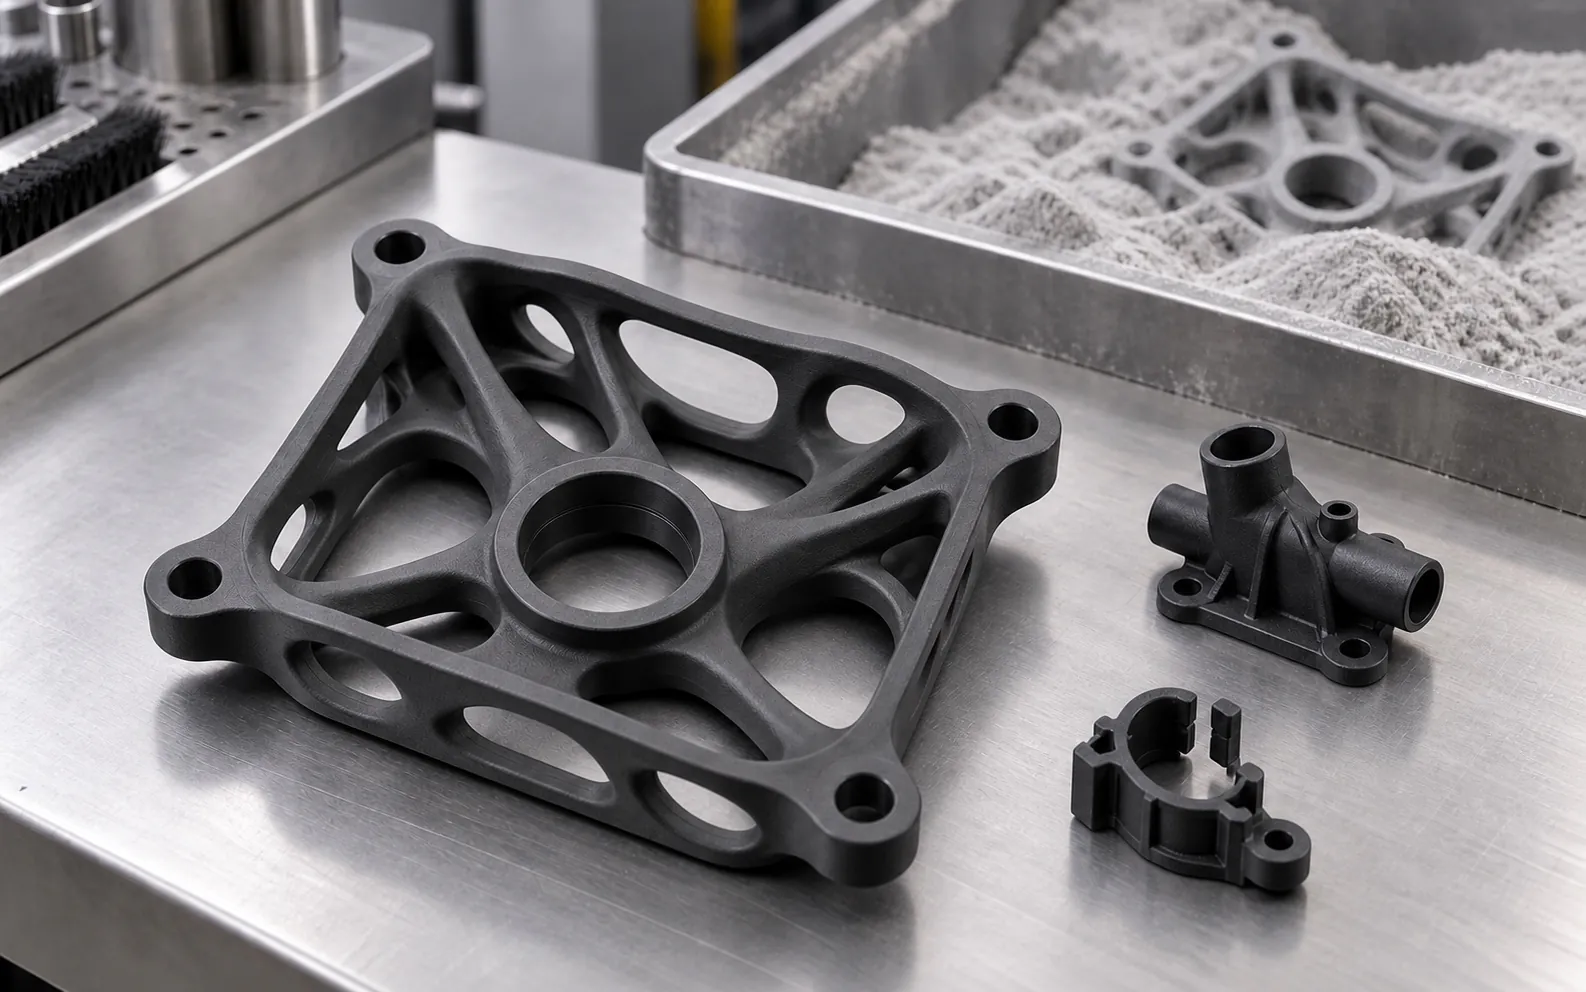
Multi Jet Fusion · SLA · From 1 unit
Functional parts with HP Multi Jet Fusion in five materials, and aesthetic parts in white, black or clear SLA resin. No molds, straight from your 3D file.
01 / How it is printed
HP Multi Jet Fusion for functional parts. Stereolithography for aesthetic parts. Choose based on what the part has to do.
MJF · HP Multi Jet Fusion
Housings, clips, ducts and fixtures with end-use part properties. Five materials: PA12, PA11, PA12 GB, PP and flexible TPA.
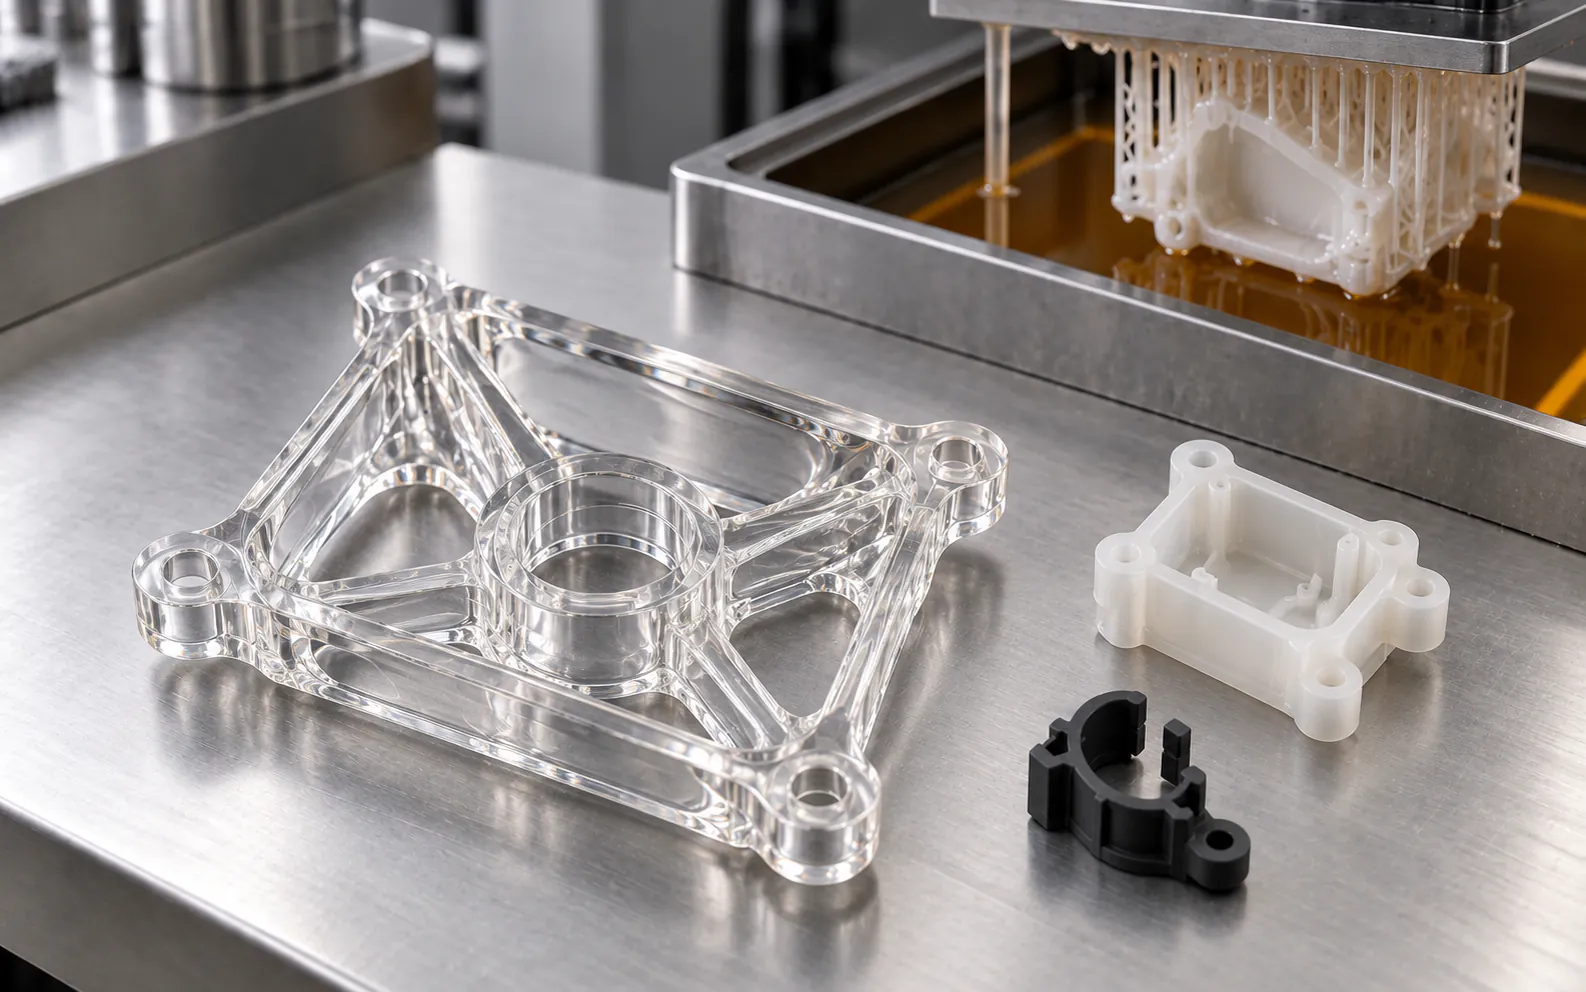
SLA · Stereolithography
Mockups, parts for painting and clear housings. Three resins: white, black and clear. The resin deforms at 45–50 °C: functional parts go in MJF.
MJF · Step by step
The unfused powder holds the part during printing. Afterwards, it is removed and the part is cleaned, without supports to cut.
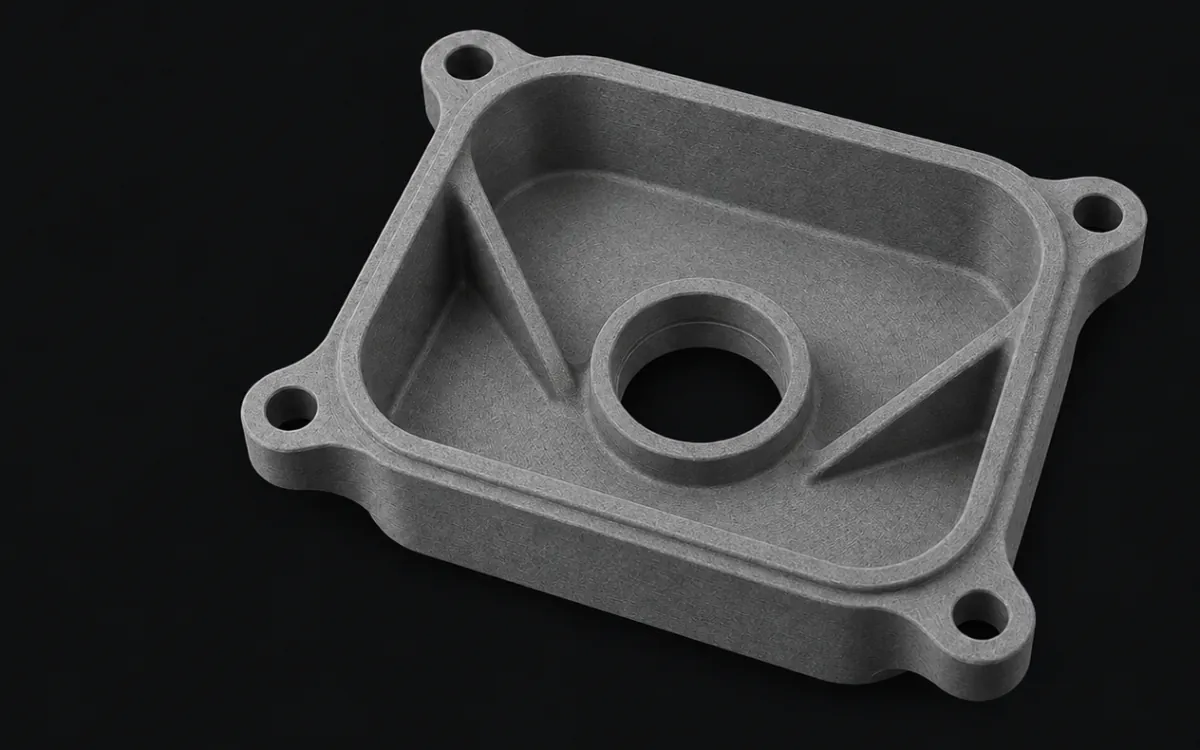
The 3D view requires a browser with WebGL.
A roller spreads a thin layer of PA12 powder over the platform.
02 / Materials
Multi Jet Fusion for functional parts. Stereolithography for aesthetic parts. Tell us what your part has to do and we will tell you which to choose.
1What is the part for?
2What does it need to meet? Check all that apply
We recommend
PA12 · MJF
Rigid and tough. The starting option: it covers most functional parts.
8 of 8 materials fit
View datasheetPA12 Nylon
Rigid and tough. Resists wear, oils, and greases.
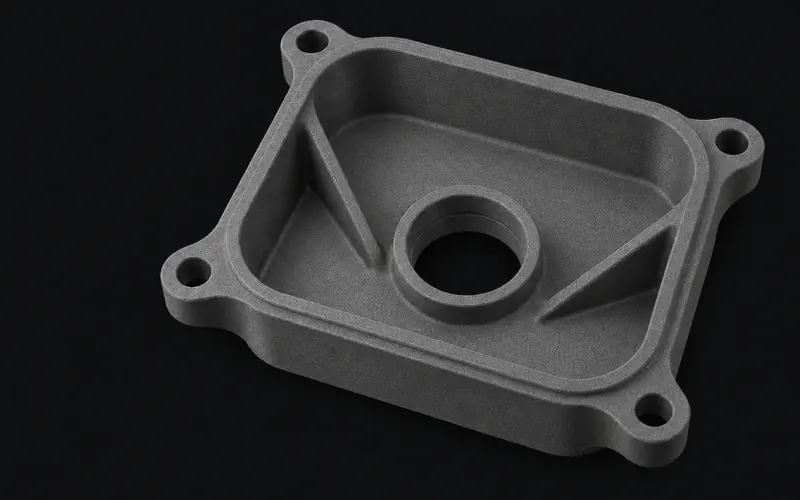
PA11 Nylon
Bends before it breaks. Handles impacts, clips, and hinges better than PA12.
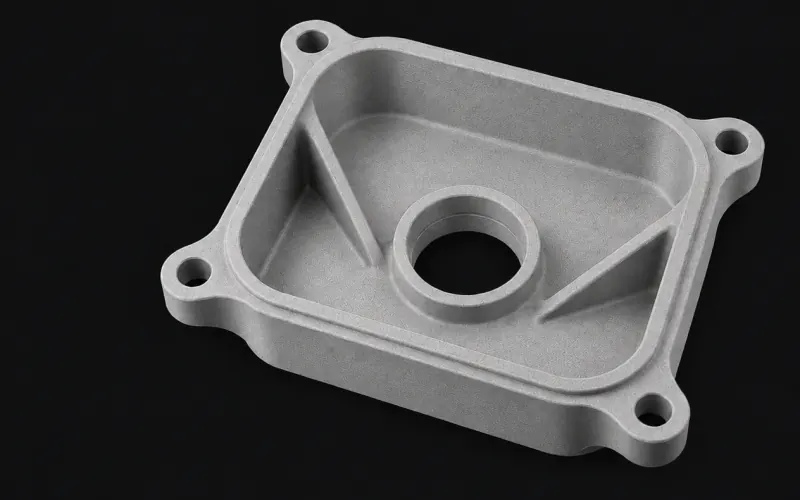
PA12 GB · glass beads
With 40% glass beads: stiffer and more stable, it does not warp or give way under heat.
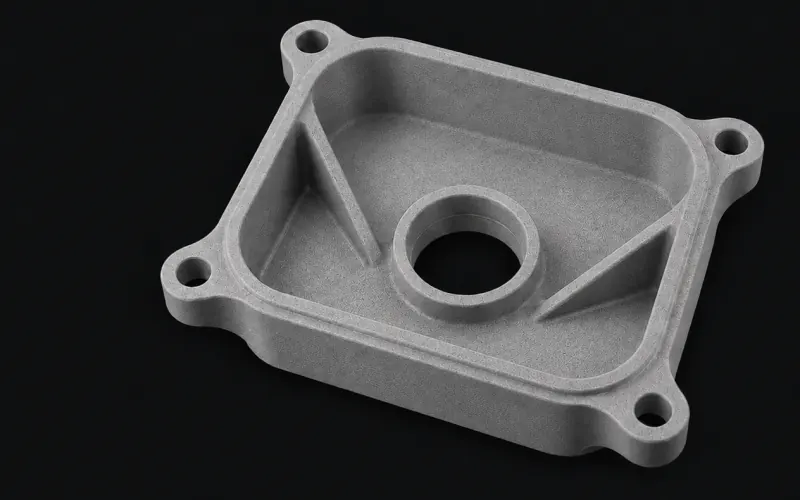
PP Polypropylene
Lightweight, watertight, and chemical resistant. Can be welded to injection-molded PP.
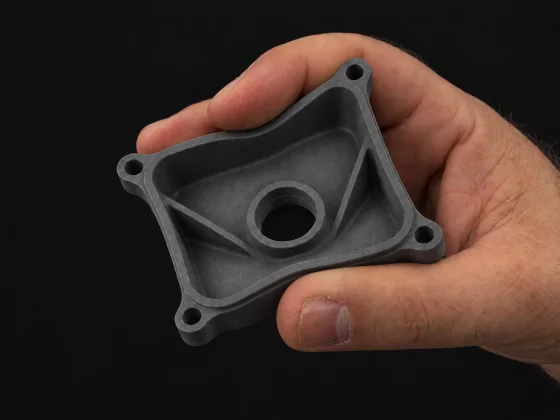
TPA 90A
Flexible like rubber. Stretches, compresses, and recovers its shape.
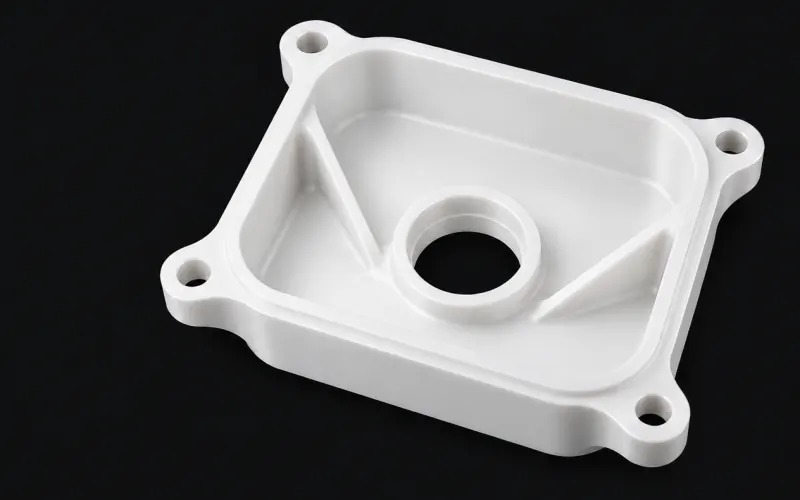
White resin
Smooth, finely detailed, and ready to paint. ABS-like.
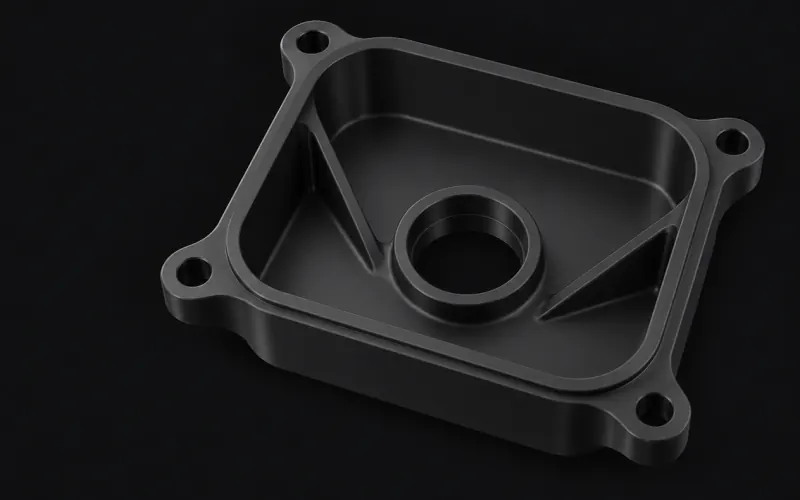
Black resin
Black throughout: show a black product without painting it. ABS-like.
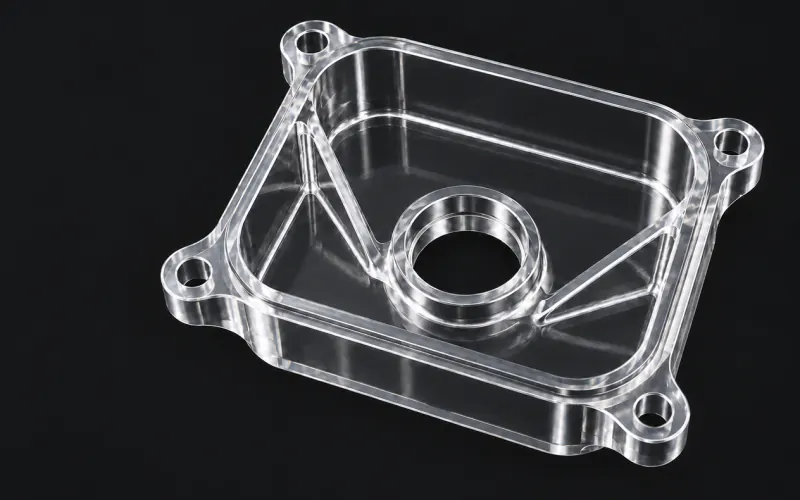
Clear resin
Nearly colorless and water resistant. Always polished, so you can see through it.
+Rigid or flexible: squeeze them.
03 / Redesign for MJF
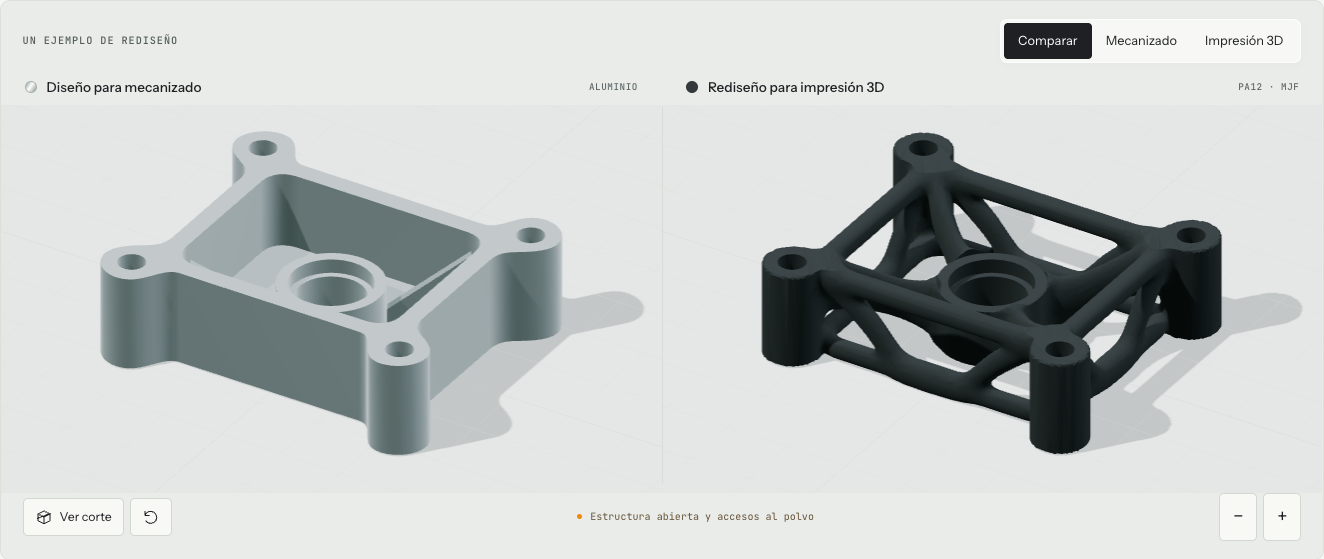
Two designs. One transformation.
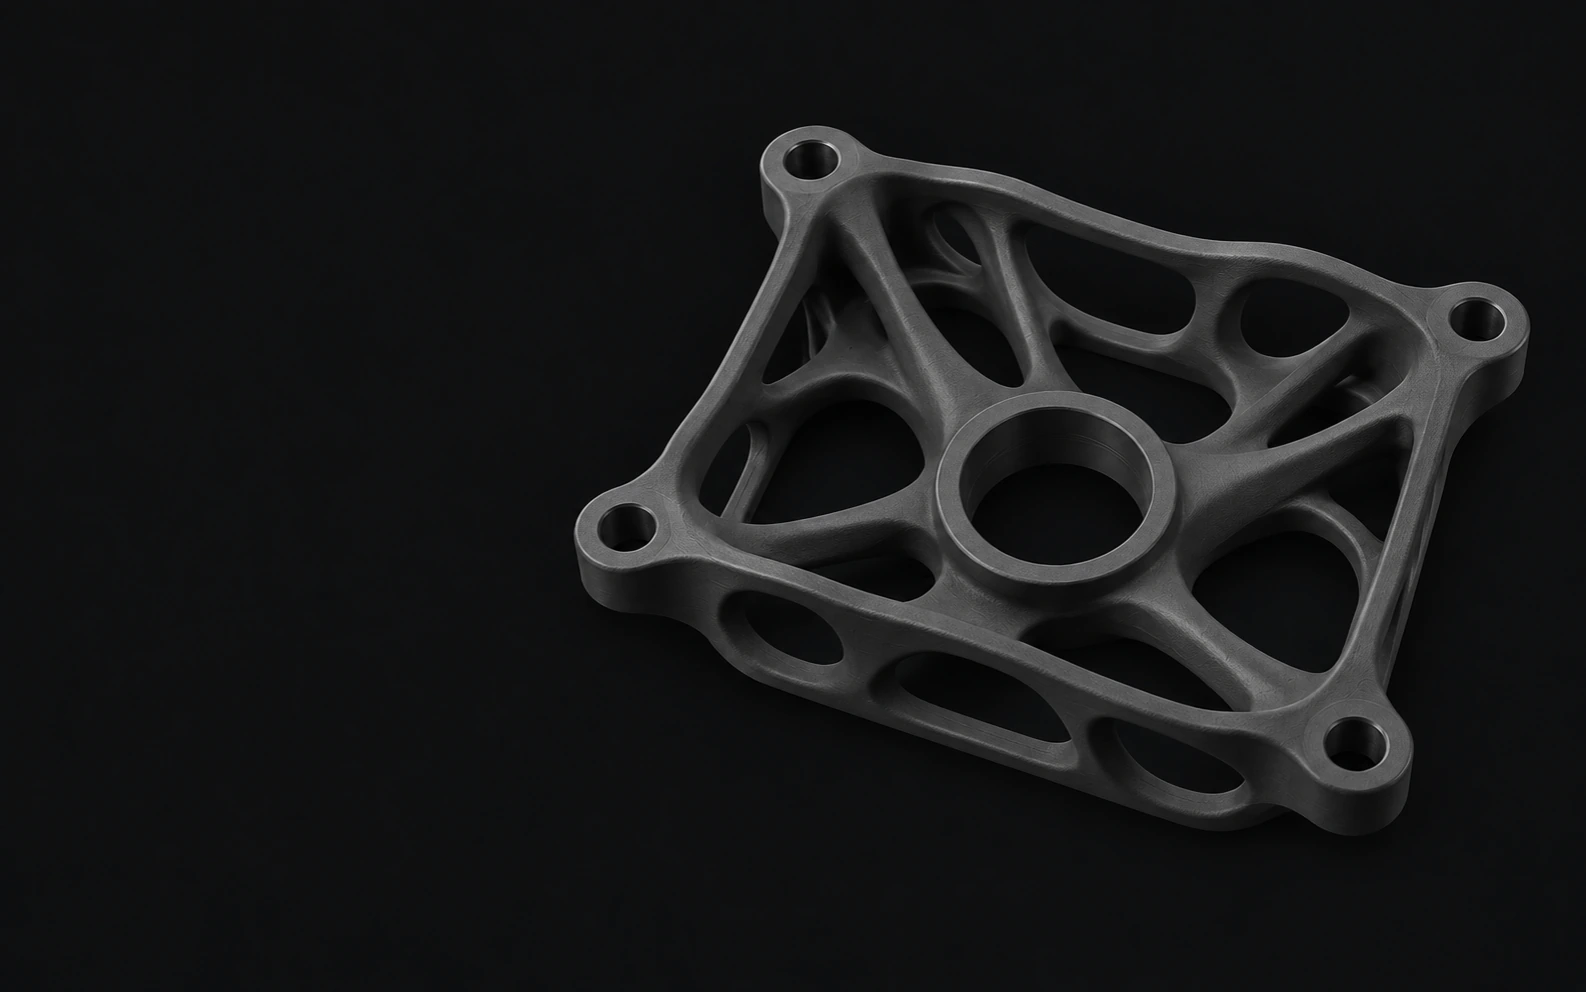
Aluminum CNC → PA12 MJF
We keep the four anchors and the central seat. We open the bottom and the walls, and connect them with curved ribs.
The result is a geometry with less material volume, designed for printing in PA12.
282 g67 g
150 €60 €
104.1 cm³66.6 cm³
Free PDF guide
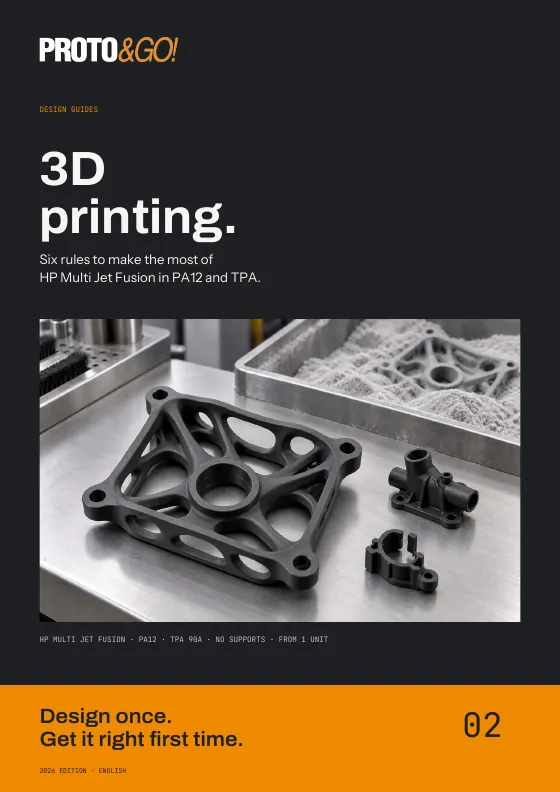
Six rules with their dimensions: wall thickness, hollowing, holes, printed threads, inserts and text. Plus when to choose PA12 or TPA, what tolerance to expect, and how to redesign for MJF a part designed for machining.
04 / Your order
Without molds or tooling: from one unit to a run using the same file.
One file per part, in STL, STEP, or your CAD format.
An engineer reviews the part and proposes material, finish, and lead time.
We verify each part and ship it to any point in Europe.
05 / Manufacturing capacity
Choose the technology: the sketch, the dimensions and the tolerance change with it.
356 × 280 × 356 mm
We leave a margin at the edges of the build chamber.Indicate on the drawing the dimensions that must be adjusted. Larger parts can be studied divided into sections.
Each technology prints on a different machine. Larger parts are assessed split into sections.
Usable area 356 × 280 × 356 mm. Tolerance ±0.3 mm up to 100 mm and ±0.3% above.
Tolerance ±0.2 mm up to 100 mm and ±0.2% above.
Tolerance ±0.2 mm up to 100 mm and ±0.2% above.
Tolerance ±0.2 mm up to 100 mm and ±0.2% above.
06 / Frequently asked questions
31 questions
The price depends on size, material volume, geometry, quantity, and finish. At Proto&Go! you upload the 3D model, specify your requirements, and receive a quote within 24 hours.
At Proto&Go! 3D printed parts are manufactured from 5 working days after order confirmation. The lead time depends on the design, quantity, and finish, and is confirmed in the quote. Shipping is added to the manufacturing lead time.
Yes. Proto&Go! manufactures via 3D printing from a single unit, without the need for molds or tooling. You can order a sample to verify the design before producing more parts.
It can be cost-effective because Multi Jet Fusion does not require manufacturing a mold. The cost depends on geometry, material, and finish. It is advisable to compare the quote for the run with other processes; quantity alone does not determine the most economical option.
Consider hollowing out solid areas, reducing material where it does not support loads, and requesting only the necessary finishes. Cavities must allow for powder removal. Savings are verified when quoting the design; lightening a part does not guarantee a proportional price reduction.
Multi Jet Fusion, or MJF, is an HP technology that manufactures parts layer by layer from polymer powder. It applies agents and heat to fuse the design areas. The part is then cooled and excess powder is removed.
They do not require added supports: unfused powder supports the part during printing. Once finished, this powder is removed. Cavities and channels must have access points to allow cleaning.
It is a technology that hardens liquid resin with a UV laser, layer by layer. The part comes out smooth and finely detailed, but it is printed on supports that are removed by hand and it gets a final cure. At Proto&Go! we offer it in white, black, and clear resin.
If the part is functional, MJF: it withstands loads, impacts and temperature. If it is aesthetic, SLA: it comes out smooth, takes paint and can be clear, but the resin deforms at 45–50 °C. The material selector settles it in two steps.
MJF 3D printing lets you manufacture complex geometries without a mold, in polyamides, polypropylene, or flexible TPA. CNC machining offers more metal and engineering plastic options and allows tighter fits. Choose based on the material, loads, tolerances, and finish the prototype needs.
3D printing allows you to manufacture and modify housings without creating a mold. Vacuum casting allows you to obtain polyurethane copies with various hardness levels, colors, and finishes. Compare both options based on quantity, material, and final appearance on the vacuum casting page.
Eight, in two technologies. With HP Multi Jet Fusion, for functional parts: PA12, PA11, PA12 GB, PP, and flexible TPA. With SLA, for appearance prototypes: white, black, and clear resin.
PA12 is suitable for rigid parts such as housings, supports, and assembly fixtures. TPA allows you to manufacture parts that compress or flex, such as bellows, protectors, and grips. The choice depends on the required rigidity, loads, and deformation.
PA12 is stiffer and more economical: it is the starting point. PA11 stretches up to 50% before breaking, versus 20% for PA12, so it handles impacts, clips, and hinges better. If the part has to flex, PA11.
It is PA12 with 40% glass beads. It is 40% stiffer, warps less, and at 1.82 MPa withstands 114 °C before deforming, versus 95 °C for PA12. It stretches only 10%: it is not suitable for clips or hinges. It works well for tooling, gauges, and brackets near heat.
90A indicates the nominal Shore A hardness of the TPA. The flexibility of the part also depends on the wall thickness and geometry: a thin wall flexes more than a block of the same material. To verify the feel and deformation, it is advisable to validate a sample.
MJF parts, yes, if the material and design meet the conditions of use: PA12 and PA11 in housings and fixtures, PP in contact with chemicals, TPA in flexible elements. SLA resin parts are for prototypes and models: they deform at 45–50 °C. Before manufacturing the run, check loads, temperature, wear, and chemicals.
PA12, PA11, and PA12 GB, in natural gray or black dyed; dyeing changes the color and keeps the texture. PP and TPA, natural gray only: PP cannot be dyed. In SLA, white and black resin can be painted (black is already dyed throughout), and clear resin is always delivered polished.
Yes, in clear SLA resin. It is always delivered with clear polish, included in the price: without it, the part remains translucent. Interior cavities that cannot be polished remain translucent. MJF materials are opaque.
In MJF, the build chamber measures 380 × 284 × 380 mm, with a recommended usable area of 356 × 280 × 356 mm. In SLA it depends on the resin: white up to 1,650 × 760 × 580 mm, clear 780 × 780 × 540 mm, and black 580 × 580 × 380 mm. See the build dimensions; larger parts are studied divided into sections.
The Proto&Go! reference for MJF is ±0.3 mm for dimensions up to 100 mm and ±0.3% above that. On a 200 mm dimension, that equals ±0.6 mm. In SLA it is ±0.2 mm or ±0.2%. If an area must fit with another part, specify the required tolerance so it can be reviewed before manufacturing.
For small PA12 walls, 1–1.5 mm is a starting point. Increase the thickness or add ribs if they are tall, long, or load-bearing. It is not a universal minimum: the design is reviewed based on geometry and application.
Yes, but it requires accessible exits to remove internal powder. For a simple PA12 housing, this guide references 2–3 mm walls and two opposite exits of Ø5 mm or more. A closed cavity retains powder and does not remain empty.
For simple holes in PA12, Ø2 mm is a recommended reference. Long or complex ducts may require a larger diameter or cleaning access. If the hole must fit a pin, specify the tolerance and consider subsequent drilling or reaming.
Yes, by modeling the full thread profile. Large threads resolve better than small ones; for M6 and smaller, consider inserts or subsequent threading. Specify metric and pitch and check the assembly with a sample before producing the run.
Yes. Inserts allow the use of metal threads in parts that are repeatedly screwed. Dimension the housing according to the insert datasheet, leave sufficient material around it, and ensure access for installation. Specify the reference and position when requesting the quote.
Yes, by incorporating it into the 3D model. As a reference, use letters of at least 2.5 mm height, strokes of 0.5 mm or more, and 1 mm relief or engraving. Small details must be checked against the final finish, as cleaning can soften their edges.
You can request them on the Proto&Go! platform, part of the i-mas group. Upload a file per part and specify material, finish, and quantity. An engineer reviews the design and you receive a quote within 24 hours. We ship parts to Spain and the rest of Europe.
Proto&Go! accepts STL and STEP for 3D printing, in addition to SLDPRT, X_T, X_B, IPT, CATPART, PRT, SAT, and 3DM. Upload a file per part. The STL format is supported for 3D printing; for other processes, a compatible CAD format is required.
To quote and manufacture, a 3D model is required. If you only have a drawing or a sketch, consult the i-mas engineering team to evaluate creating the model before requesting manufacturing.
The 3D file is the basis for reviewing the part. Attach a PDF if you need to specify specific tolerances, threads, inserts, or requirements not described by the model. Also specify material, quantity, and finish when requesting the quote.
Try another word or select «All» to search across all topics.
07 / Guides
How an MJF printer works, what post-processing the part gets, when the prototype is already the final part and how to avoid warping.
All 3D printing articles3D printing
Choose material, finish, and quantity on the platform. You get the quote in 24 hours.
It opens in a new tab. Accepted formats:
We use our own and third-party cookies to understand how the website is used and which campaigns work. You can accept them all, reject them all or choose which ones; the website works the same either way. Cookie policy.