Price, quantities, and lead time
How much does it cost to manufacture parts via vacuum casting?
The price depends on the master, silicone molds, polyurethane volume, complexity, and finish. When producing multiple units, the initial cost of the master and the mold is distributed. At Proto&Go! you upload the 3D model, specify quantity and finish, and receive a quote within 24 hours.
I need 50 or 100 plastic housings: which process suits me best?
Vacuum casting is an option for short runs of housings with a final product appearance. It allows obtaining polyurethane copies using a silicone mold and choosing color and finish. It is advisable to compare it with 3D printing and injection molding based on geometry, material, tolerances, and quantity; the number of parts alone does not decide the process.
How many parts can be manufactured with a silicone mold?
In this guide, we use a reference of about 20 copies per mold. The actual duration depends on the geometry, the resin, and the demolding operations. For a run of 100 parts, several molds may be required; their number is confirmed upon reviewing the design.
What is the lead time for vacuum casting parts?
At Proto&Go! you receive the quote within 24 hours and parts are manufactured starting from 10 working days. Quantity, material, molds, and finishes can change the lead time. The date applicable to your order is indicated in the quote.
How can I reduce the price of a short run of polyurethane parts?
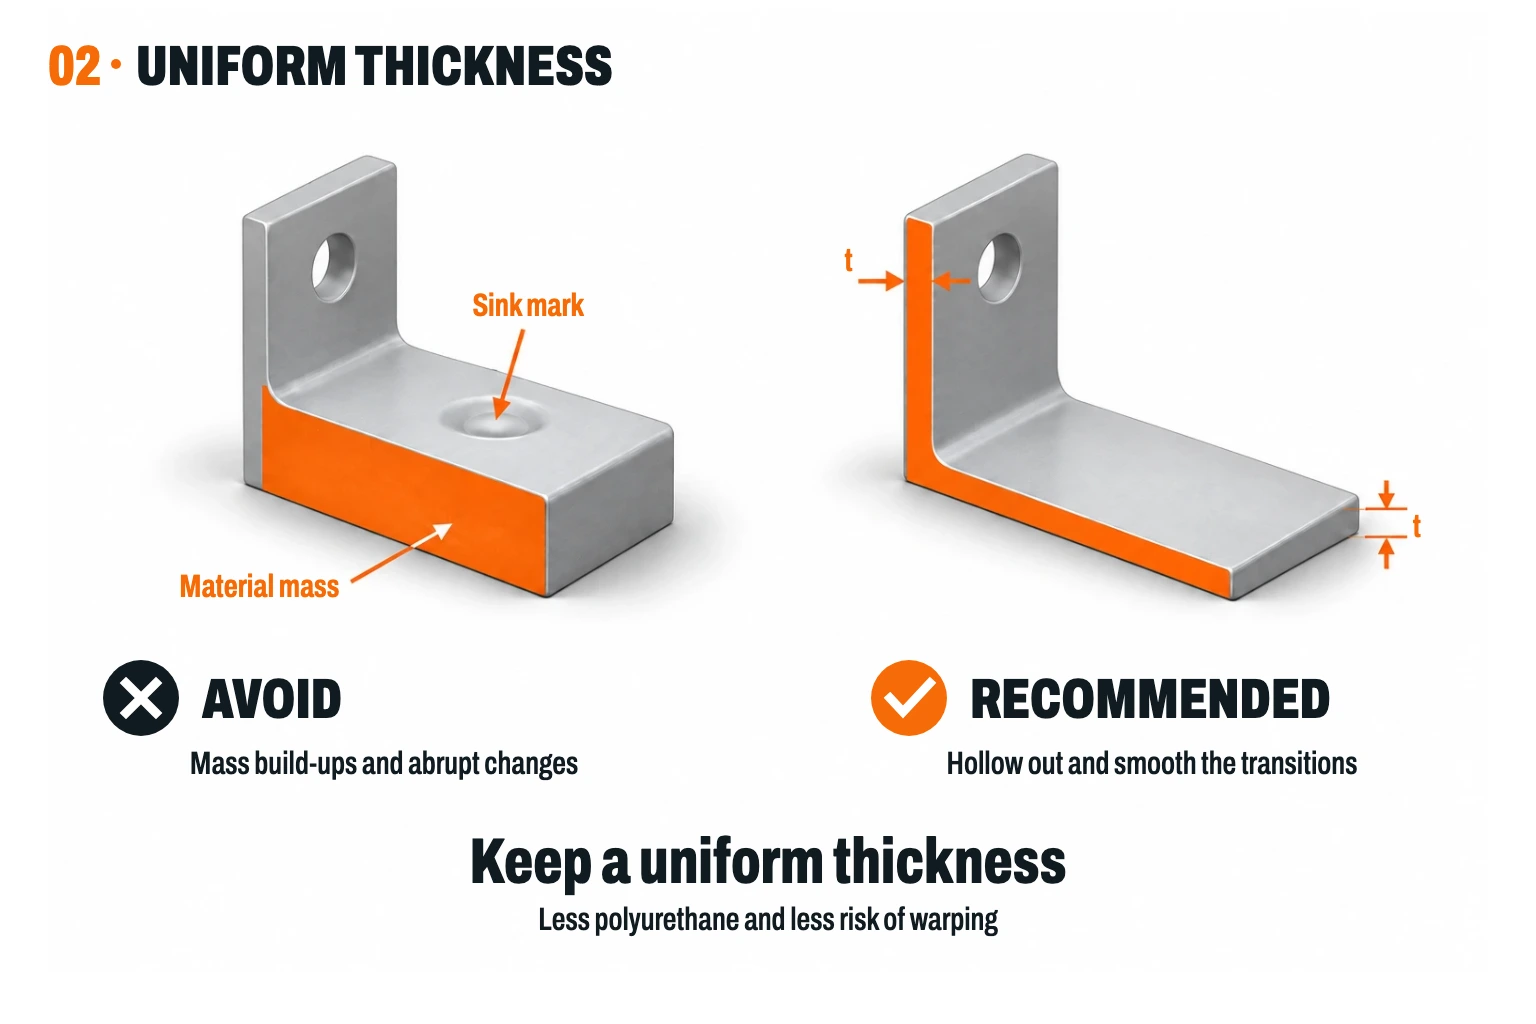
Maintain uniform wall thicknesses, avoid unnecessary solid volumes, and simplify undercuts that hinder demolding. Comparing quantities helps distribute the cost of the master and the molds. If the required appearance allows it, bulk pigmentation can avoid preparation and painting operations.
Can a single part be manufactured via vacuum casting?
It is technically possible, but making a master and a mold for a single copy may not be cost-effective. For a single unit, compare machining and 3D printing. Vacuum casting makes sense when you need several copies with the same appearance or a specific PU resin.
Process and material selection
What is vacuum casting and how are parts manufactured?
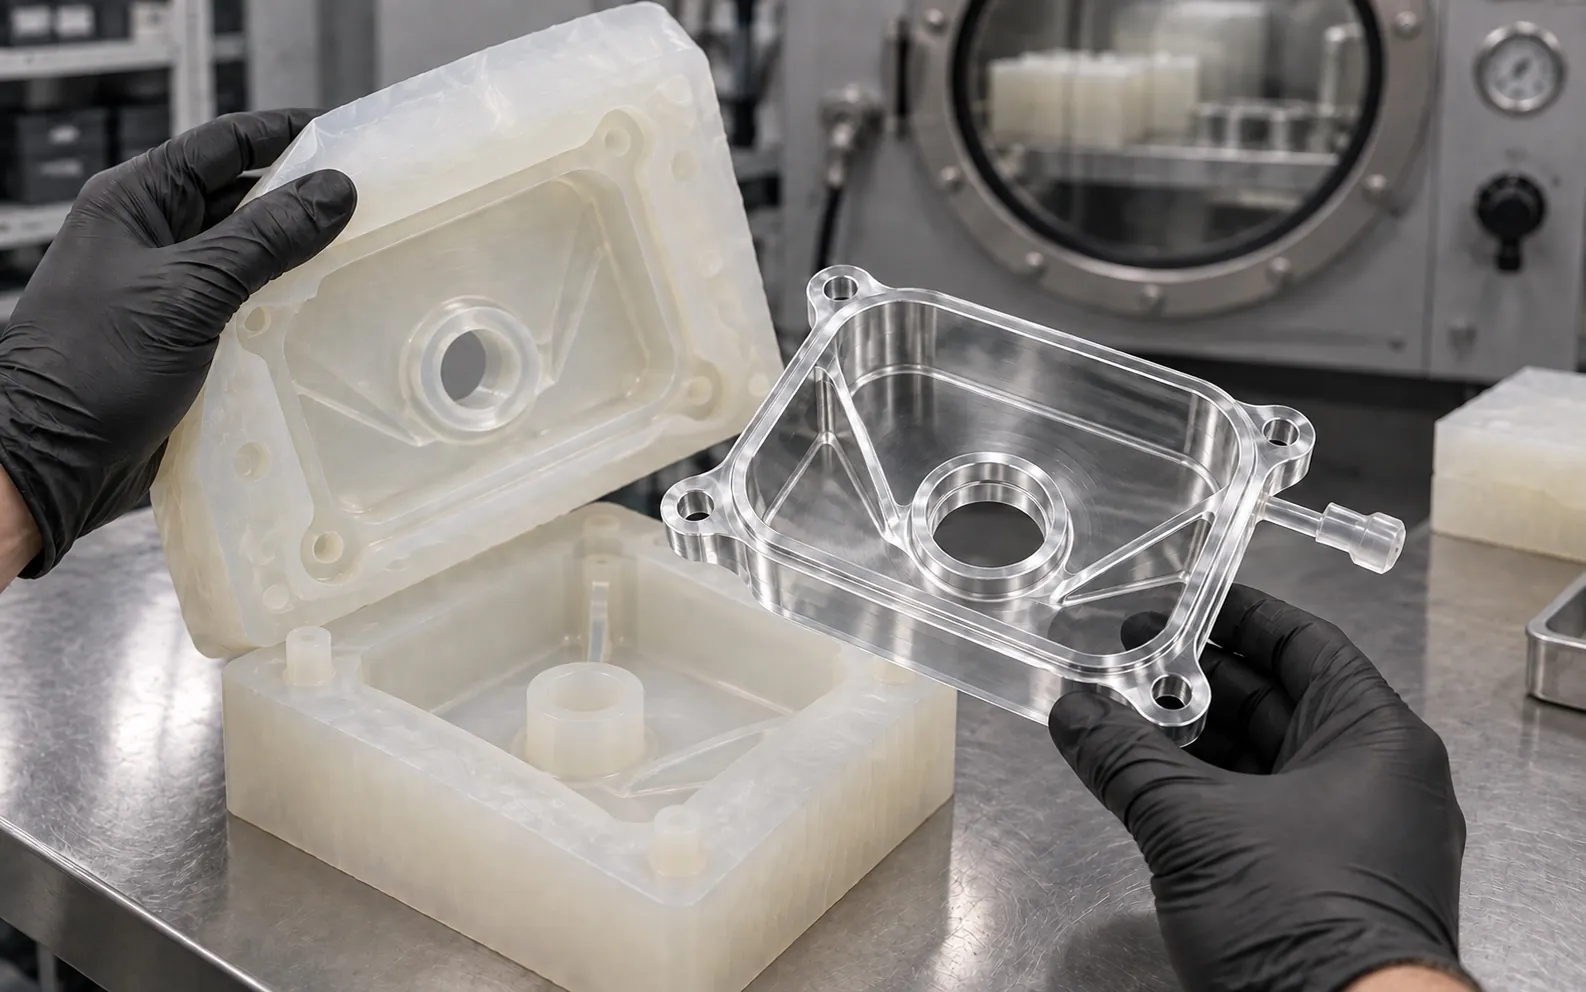
Vacuum casting reproduces a master pattern in a silicone mold. Liquid polyurethane is prepared, the mold is filled under vacuum to reduce trapped air, and it is left to cure before demolding. At Proto&Go!, we machine the master to ensure the surface that the mold and parts will subsequently copy is properly finished.
Vacuum casting or plastic injection for a short run?
Vacuum casting uses silicone molds with lower initial investment and a limited lifespan. Injection molding uses a metal mold whose cost is better distributed as the run increases. The choice also depends on the final material, tolerances, and repeatability: request a comparison for your design and expected volume.
Vacuum casting or 3D printing for presenting a functional prototype?
3D printing allows iterating geometries without manufacturing a mold. Vacuum casting is useful for obtaining multiple PU copies with texture, color, and feel close to the intended product. For a functional test, compare the datasheet of each material with loads, temperature, and real usage conditions.
Is ABS-type polyurethane really ABS?
No. It is a polyurethane formulation whose properties aim to approximate some of those of ABS. The same applies to PC-type, PMMA, silicone, or TPE references. If you need the exact production material, a certification, or a specific property, you must check the datasheet and consider another process.
Can I use vacuum casting parts as the final product?
Yes, when the PU formulation and the design meet the usage conditions. Load, temperature, solar exposure, chemical agents, wear, and service life must be reviewed. Strength or durability cannot be deduced solely from the process or its resemblance to another plastic.
Where can I order a short run of polyurethane parts in Spain?
At Proto&Go!, the manufacturing platform of the i-mas group. You can upload the 3D model, specify material, color, and quantity, and receive a quote within 24 hours. The team reviews the part and performs quality control before shipping.
Hardness, color, and transparency
Can flexible joints, bellows, or grips be manufactured via vacuum casting?
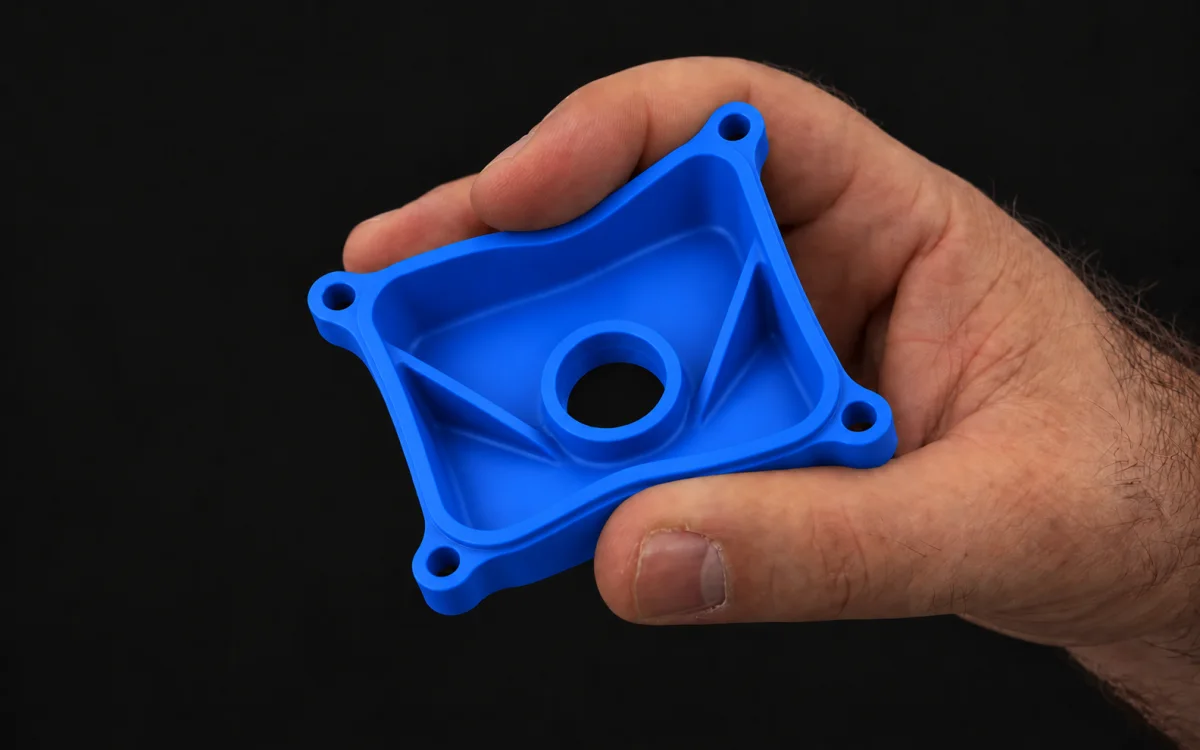
Yes, these parts can be studied in flexible PU, with hardness between 30 and 90 Shore A depending on the formulation. Hardness is selected along with wall thickness, required deformation, and tear resistance. For joints or bellows, recovery after compression and fatigue must also be validated.
What does Shore A mean and how do I choose the hardness of a flexible part?
Shore A measures the elastomer's resistance to penetration by a durometer. Within this scale, 30 A is softer than 90 A. The choice depends on how much the part must deform, its geometry, and the loads: two parts with the same hardness may flex differently if the thickness changes.
What real-world examples exist for Shore A 30, 50, 70, and 90?
There are 30 Shore A silicone suction cups, such as VacMotion SB53-SIT30; 50 A EPDM bumpers, such as the EPDM Rubber Bumper from Kast Rubber; 70 A O-rings, such as Parker N0674-70; and 90 A NBR support rings, such as Parker Parbak N0300-90. The material selector includes an example for each 5-point step. These are examples of hardness, not performance equivalencies with PU.
What is the difference between pigmented and painted polyurethane?
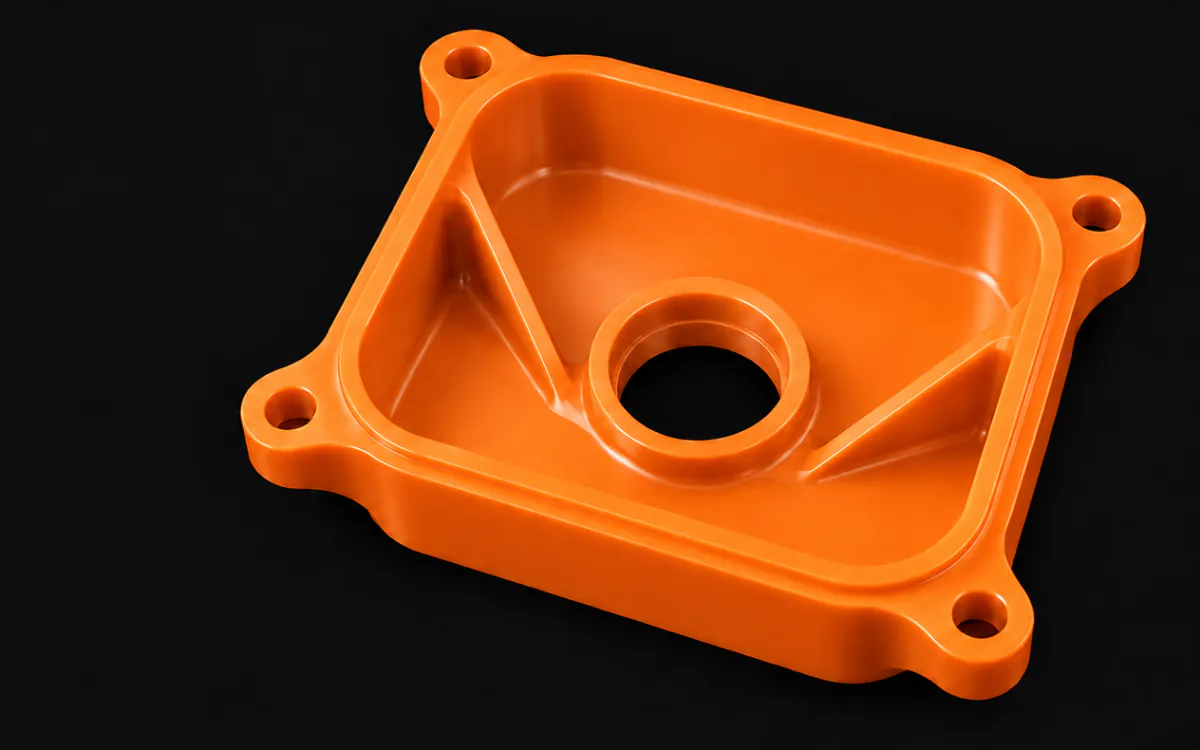
In pigmented parts, the color is mixed with the resin before casting and remains throughout the thickness. In painted parts, a paint layer is applied to the already manufactured part. Pigmentation maintains color under a surface scratch; paint allows defining the exterior appearance, but a scratch that penetrates the layer may reveal the base material.
What finish is suitable for a part that will undergo rubbing?
Bulk pigmentation prevents a scratch from exposing an interior layer of a different color. Still, rubbing can leave marks and change the gloss. Wear resistance depends on the PU formulation and contact conditions, so it is advisable to test the material if friction is continuous.
Can I order polyurethane parts in a RAL or Pantone color?
Yes, a RAL or Pantone reference can be used for pigmentation or painting. Pigmentation has a tone tolerance, and a screen image does not validate the final color. For visible surfaces or brand colors, indicate the reference and the gloss level.
Can I choose matte, satin, or glossy for both pigmented and painted parts?
Yes. In a pigmented part, gloss and texture depend on the surface finish reproduced by the master and the mold. In a painted part, they also depend on the applied paint system. These are distinct decisions: first, choose how to incorporate the color, and then the surface appearance.
Can rigid or flexible transparent parts be manufactured?
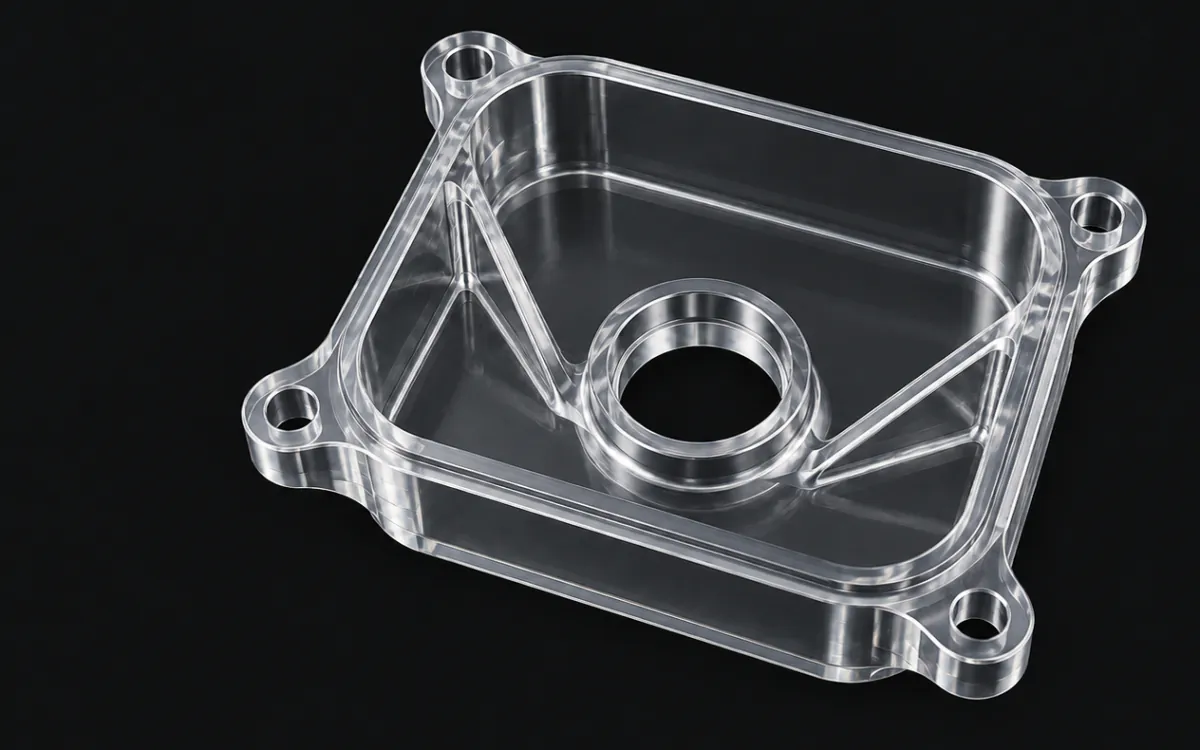
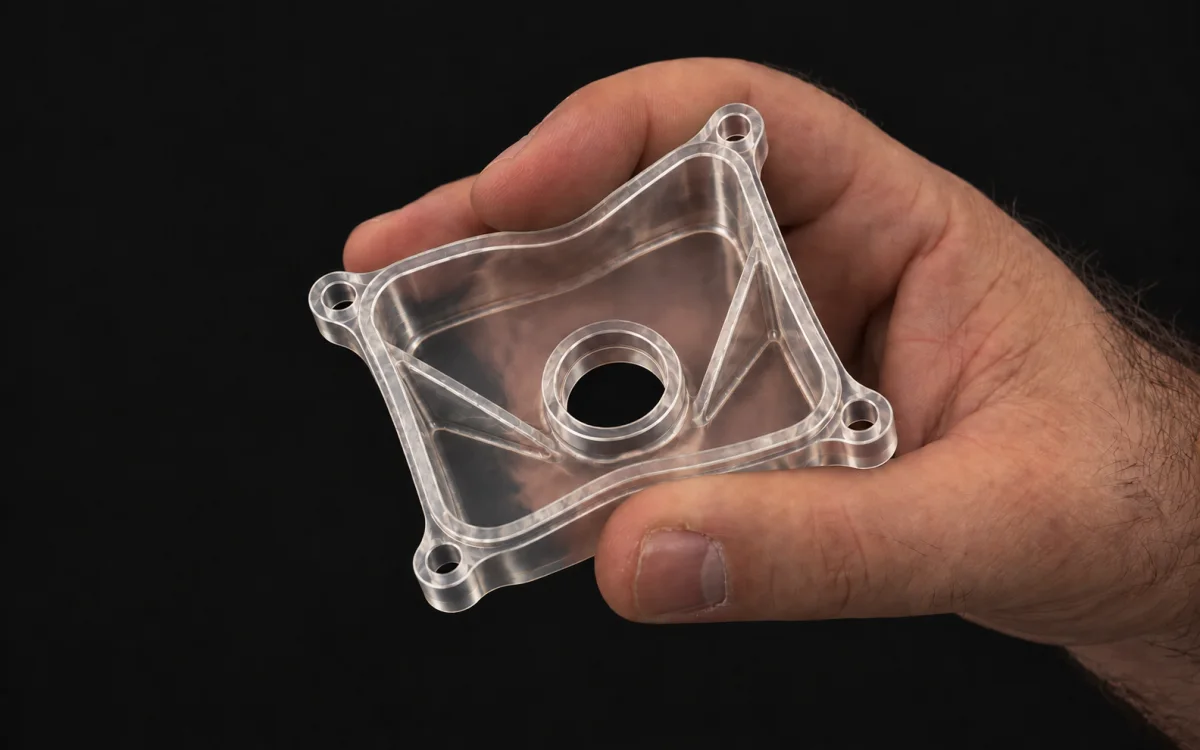
Yes, there are rigid transparent PU and flexible transparent PU formulations. Clarity depends on the material, wall thickness, and mold surface. The combination of transparency and hardness must be confirmed; if the part has an optical function or will be exposed to sunlight, its specific requirements must be reviewed.
Design, files, and order
What wall thickness is recommended for vacuum casting?
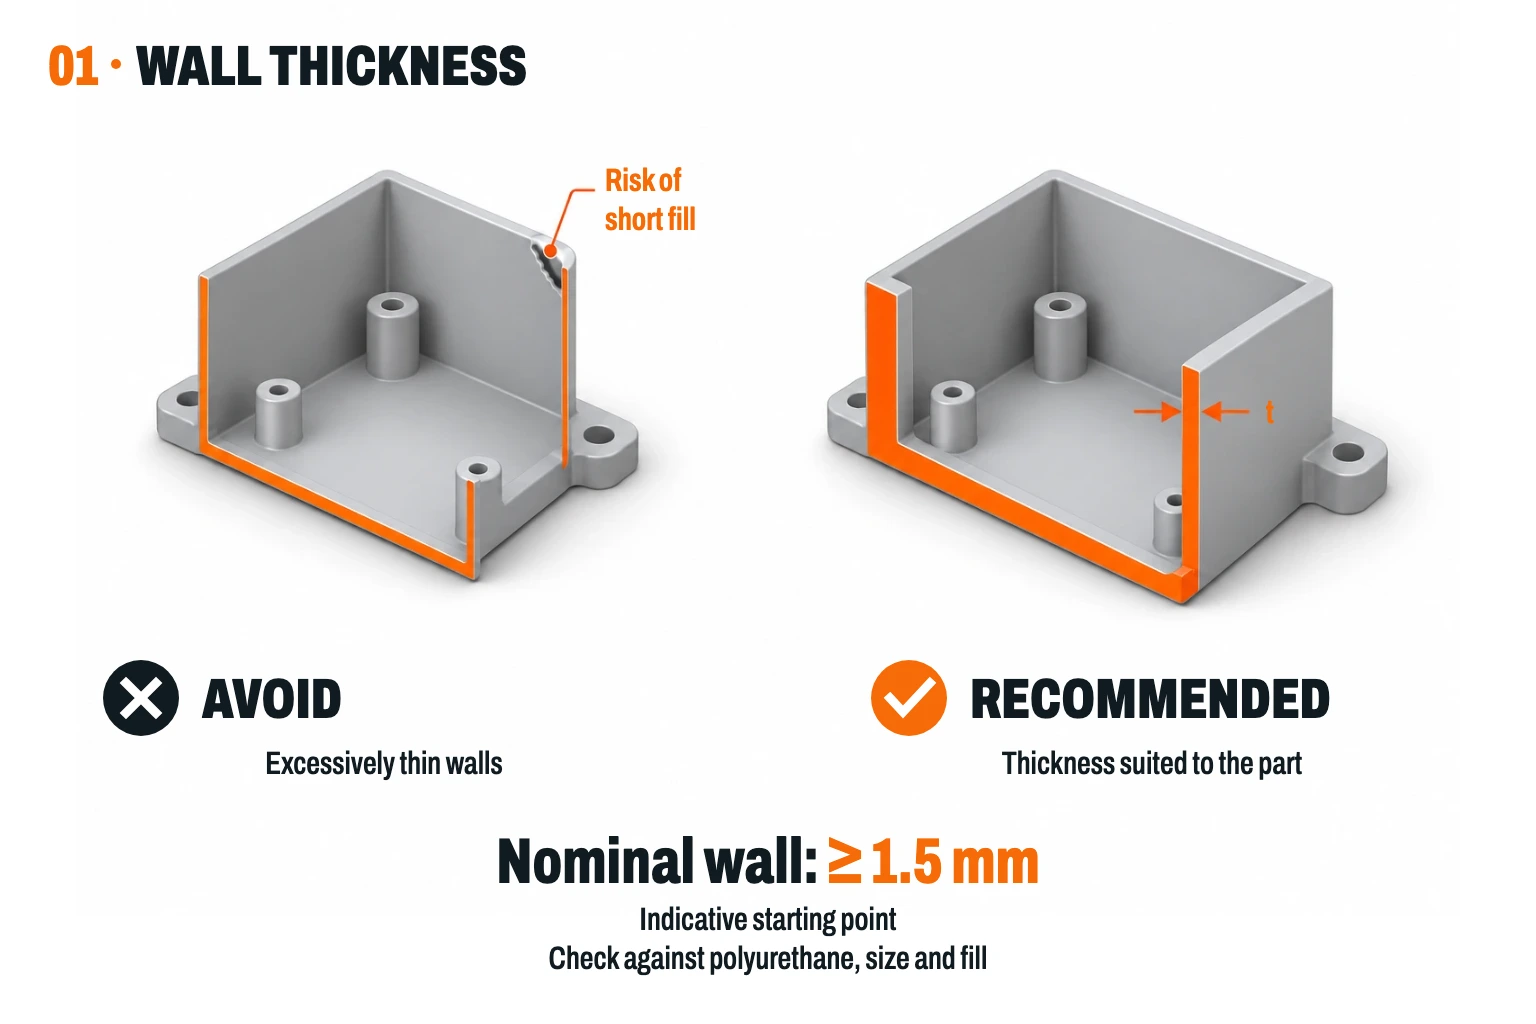
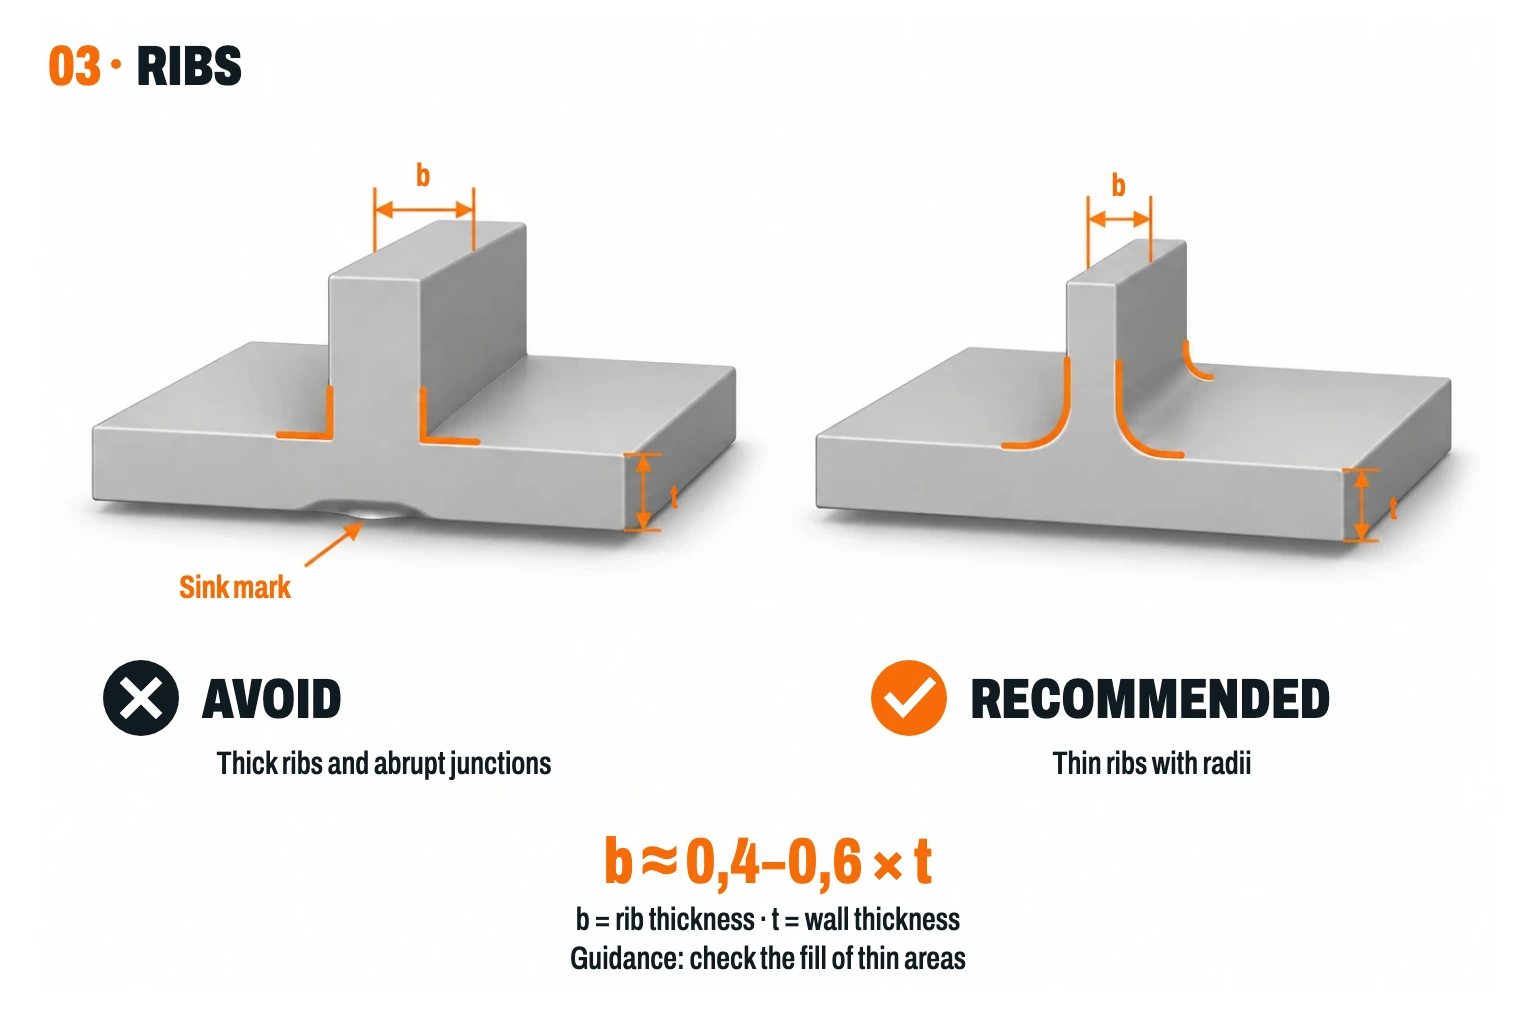
As a starting point, design a nominal wall thickness of about 1.5 mm and keep wall thicknesses uniform. Areas below 1 mm require specific review. Filling and final feasibility depend on the length of the thin zone, geometry, and polyurethane formulation.
Can undercuts and complex shapes be made with silicone molds?
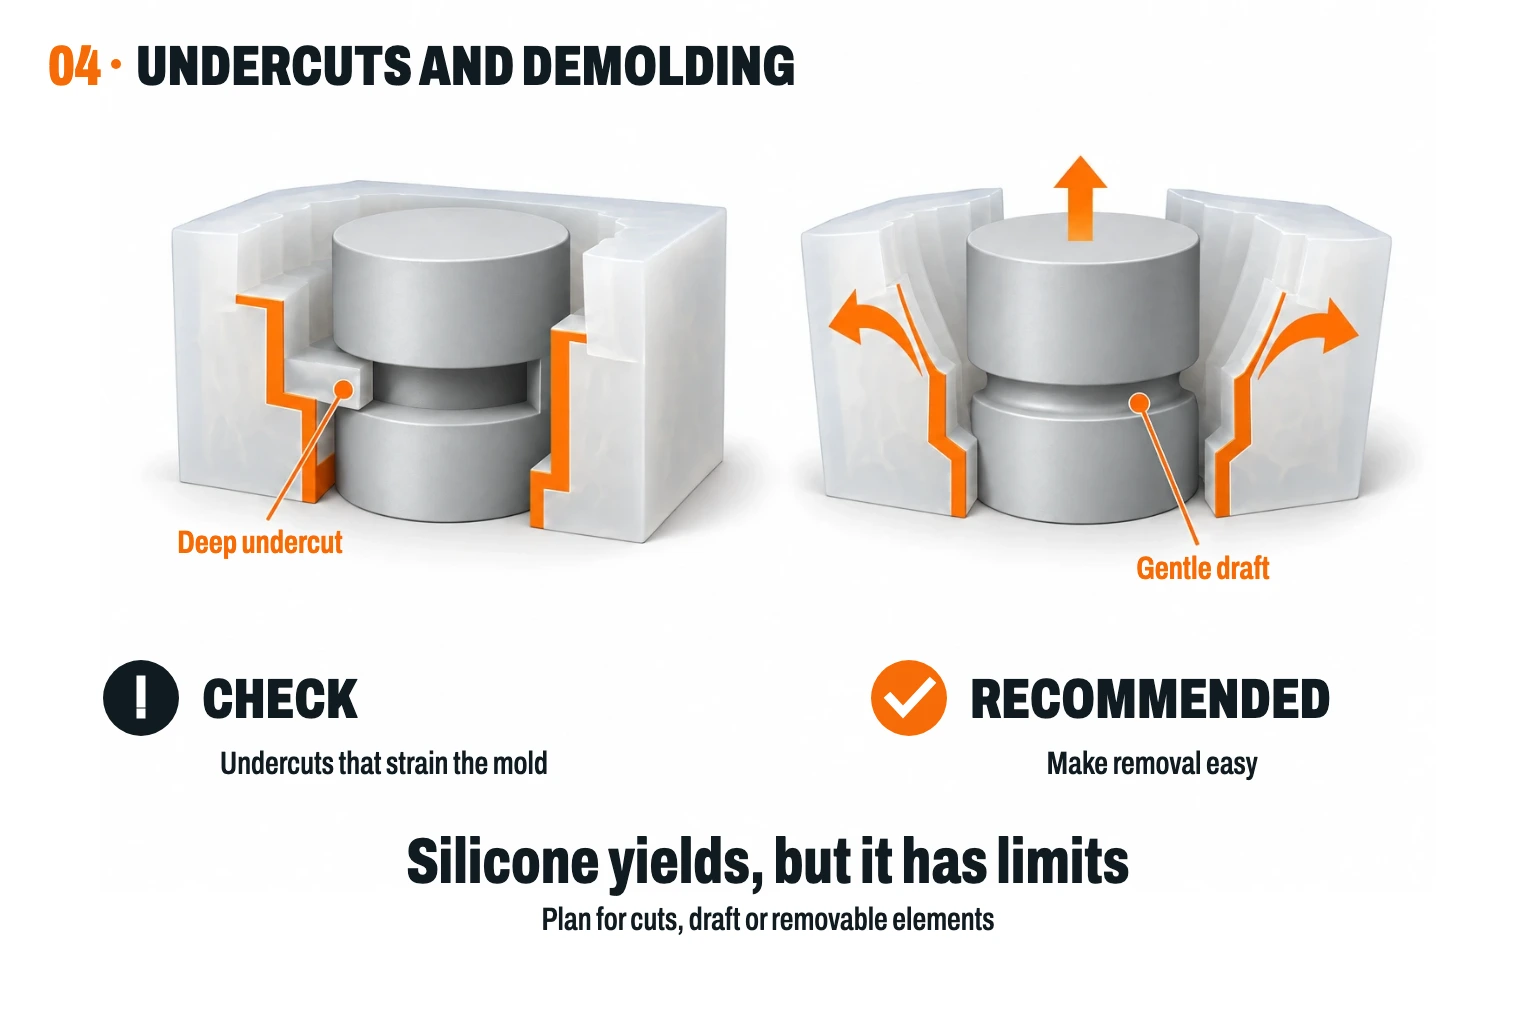
The flexibility of silicone allows many undercuts to be demolded. Deep hooks, aggressive edges, and closed zones require studying how to extract the part without damaging it or tearing the mold. Some geometries require cuts or detachable elements, which increases the work per copy.
Can I add metal inserts or threads to a polyurethane part?
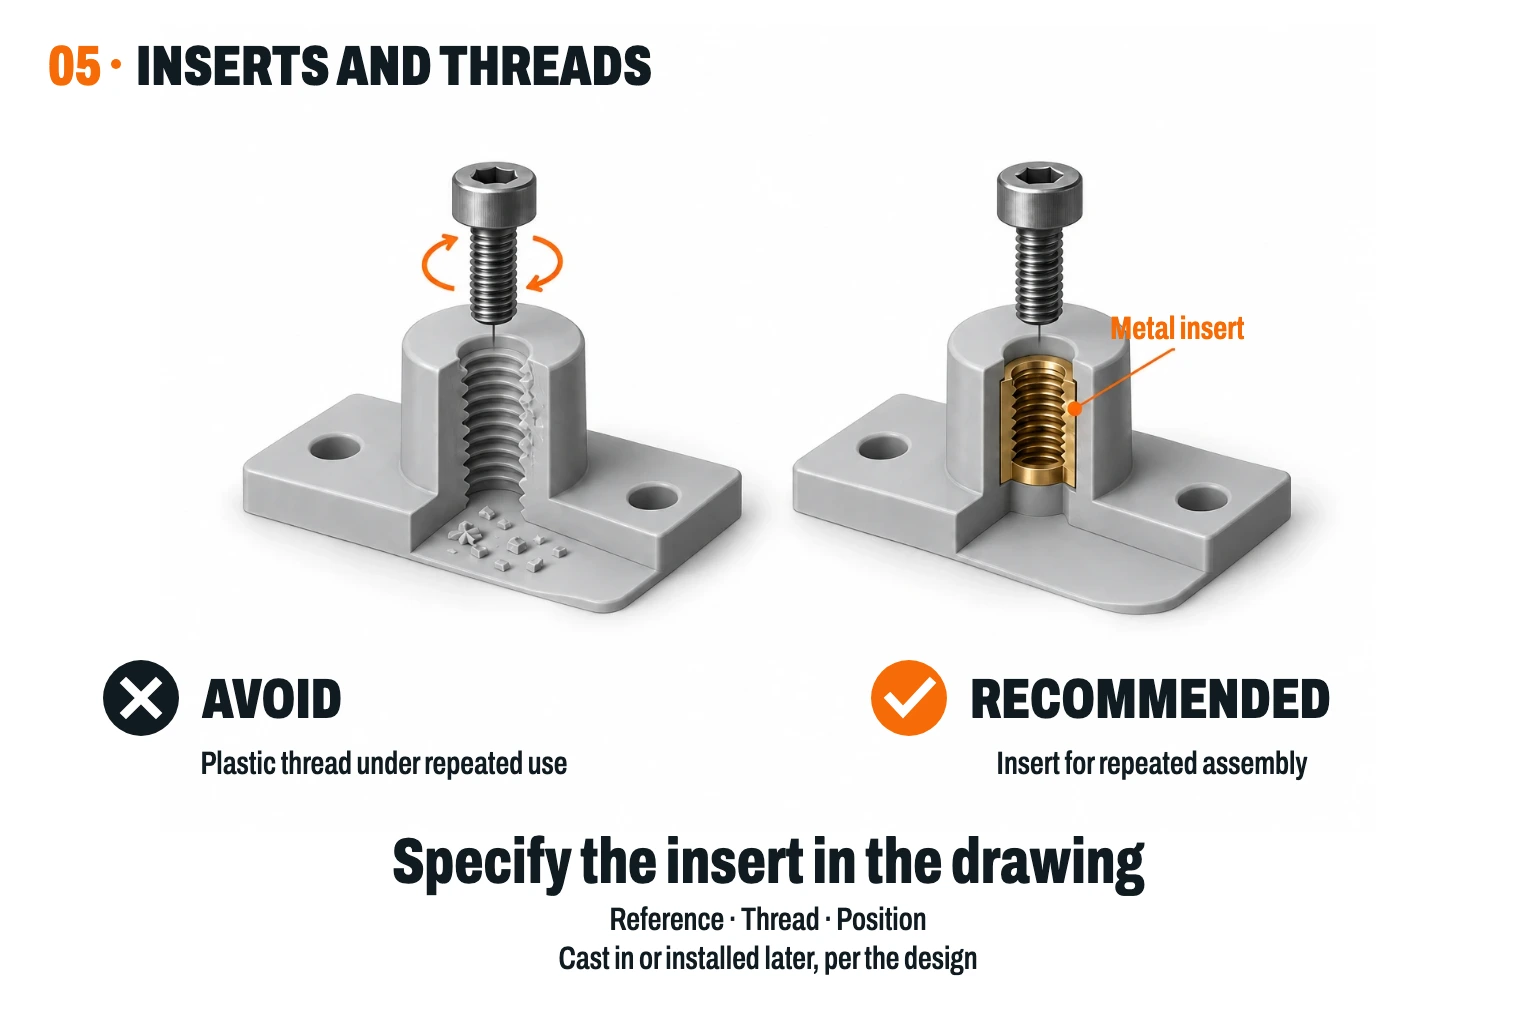
Yes. Inserts can be incorporated during casting or installed afterward, depending on the design and the PU. For repeated assemblies, a metal insert is generally preferable to a direct thread in plastic. Specify reference, metric, position, and housing in a PDF drawing.
What file do I need to order parts via vacuum casting?
Upload a 3D model per part, preferably STEP or an accepted CAD format, and indicate material, quantity, color, and finish. Add a PDF for threads, inserts, or requirements not defined in the model. At Proto&Go! we manufacture the master and molds from your design.
Do I need to send a physical part or manufacture the master myself?
It is not necessary: to get a quote at Proto&Go! just the 3D model is enough. We prepare the master and the silicone mold. If you start from a physical part and do not have a model, you must first study how to obtain the geometry before requesting a quote for the copies.
What tolerances can I request for a vacuum casting part?
The tolerances depend on the dimensions, the geometry, the resin, and the shrinkage during curing. Indicate the functional dimensions and their requirements when requesting the quote to check if the process can meet them. A visual similarity with an injection-molded part does not guarantee the same dimensional precision.