Tips for optimizing the CNC machining process and reducing its costs
What drives the price of a machined part and the seven design decisions that lower it most, in order of effect.
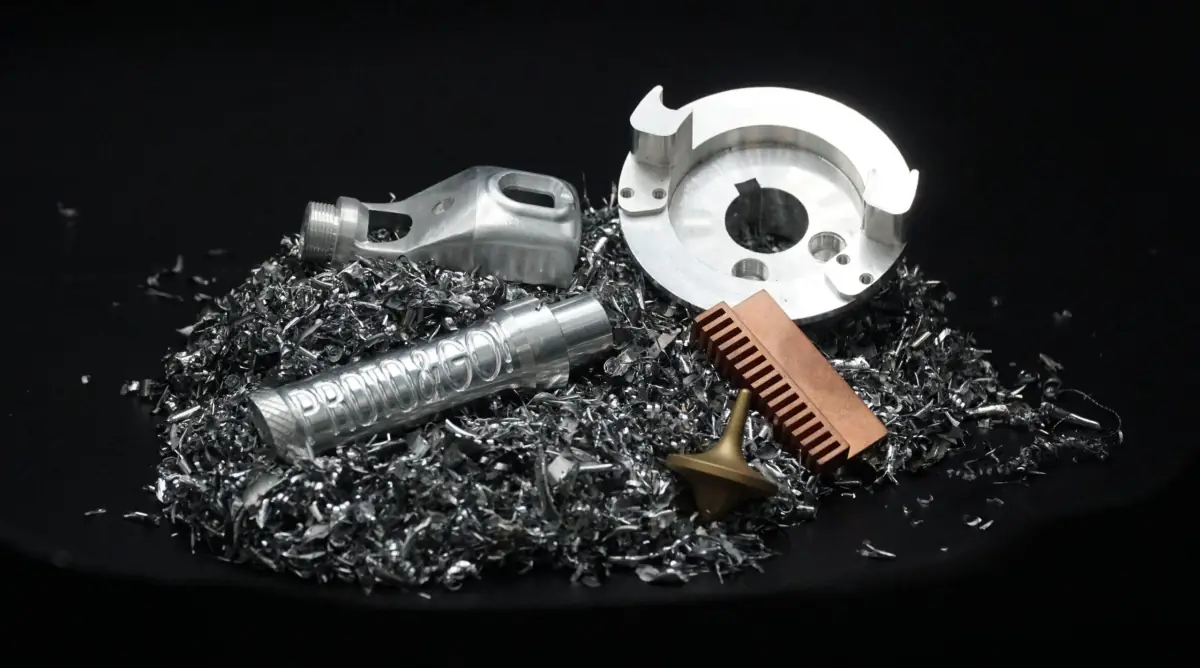
The price of a machined part is primarily CNC machining time and number of setups. Both are determined in the CAD before uploading the file. Seven design decisions (radii of 1 mm or more, shallow pockets, tolerances only where necessary, standardized drilled holes, easy-to-machine material, fewer machining faces, and the appropriate quantity) can reduce cutting time by half without changing what the part does.
This guide explains what the price depends on in CNC machining of custom parts and covers those seven decisions in order of impact, detailing how each one changes and why.
A single part pays for programming, setup, and cutting. The 10th part pays only for cutting. Design for fast cutting and order the quantity that spreads the fixed costs.
What determines the price of a machined part?
- CAM programming and setup: charged once per order. They weigh heavily on a single unit and almost nothing on twenty. We detail this in the role of CAM software in machining.
- Setups: every face machined from a different direction can be an additional setup, with its time and error risk.
- Cutting time: determined by the volume of material to remove, the smallest tool size your geometry requires, and the material hardness.
- Material: the raw stock and, above all, its machinability. Stainless steel cuts three to four times slower than aluminum.
- Tolerances and control: every refined dimension is a slow pass and a part measurement.
- Finish: charged per batch and adds to the lead time.
The minimum order is 60 € and the minimum manufacturing cost per machined part is 46 €: below that, no design optimization lowers the price further.
The seven decisions that lower the price the most
| Decision | What changes in the workshop | Effect on price |
|---|---|---|
| 1 · Internal radii of 1 mm or more | Allows large, rigid end mills, without re-cutting corners with a fine end mill | High |
| 2 · Tolerances only on functional dimensions | Avoids slow finishing passes and part-by-part measurements | High |
| 3 · Fewer machined faces | Fewer setups, less preparation, better precision between faces | High |
| 4 · Shallow pockets | Short tools, more feed, less vibration | Medium |
| 5 · Standardized drilled holes and threads | Stock tools, no special tools or extra changes | Medium |
| 6 · Easy-to-machine material | Cutting speed several times higher | Medium to high depending on the material |
| 7 · Quantity distributed by the fixed amount | Program and setup divided across more parts | High in small quantities |
1 and 4 · Internal radii and pocket depths
The end mill is round: each internal corner has the tool radius. A 0.5 mm radius at the bottom of a 25 mm pocket requires finishing with a 1 mm end mill, which advances at a fraction of the speed of a 10 mm tool and breaks easily. Design radii of at least 1 mm and one-third of the depth, and pockets shallower than three or four times their width. If another part with sharp corners must fit, add a relief at the corners instead of demanding a sharp corner. Tooling details are in different machining tools.
2 · Tolerances: the general ones are already fine
Without specifying anything, we apply ISO 2768-f in metals: ±0.1 mm on a 25 mm dimension. This is more than enough for housings, supports, and tools. A dimension to IT7 (21 µm in Ø25) can double the time for that operation; machining an entire part to ±0.02 makes it more expensive without improving performance. Set the tight tolerance only on the bearing housing or the centering pin, and leave it on the part that is easier to machine. How to write them, in CNC machining tolerances.
3 · Fewer faces, fewer setups
A plate with all the drilled holes and pockets on the top side is machined in one setup. The same plate with two side holes needs two or three. Before finalizing the design, ask for each element if it could go on the same side as the others. When it cannot, 5-axis machining does five faces in one setup, and from three setups in 3 axes, it usually comes out cheaper.
5 · Standardized drilled holes and threads
A 6 mm drill is a stock drill; a 6.3 mm drill is a special tool or a boring operation. Use standardized diameters (3, 4, 5, 6, 8, 10, 12 mm), through holes when possible, and blind holes up to 4 times the diameter. Threads from M3, with 3 thread lengths and a non-threaded margin at the bottom, and indicated in the PDF: the 3D model does not carry the metric. Each distinct hole type is one more tool and one more change.
6 · The material: machinability before raw material price
The raw material is usually a small part of the price; what weighs is the cutting time. As a relative reference, with 6082 aluminum as the base:
| Material | Relative cutting time | When to choose it |
|---|---|---|
| Aluminum 6082 / 6061 | 1 (reference) | By default for structural parts, housings, and tooling |
| Brass | ≈ 1 | Contacts, fittings, decorative parts |
| POM (Delrin) | ≈ 1 | Easy engineering plastic, guides, and gears |
| Carbon steel | ≈ 2 a 3 | Shafts, wear-resistant tooling, welding |
| Stainless steel 304 / 316 | ≈ 3 a 4 | Corrosion resistance, food industry, outdoor use |
| PEEK | ≈ 2 | Temperature and chemical resistance, only where necessary |
| Titanium | ≈ 4 a 6 | Weight and biocompatibility |
If the prototype can be validated in aluminum, do not make it in stainless steel. The 21 material datasheets, with compatible machinability and finishes, are in CNC machining materials.
7 · The quantity that keeps the price fixed
Programming, preparation, and the first setup are charged once. Between one and five units, the price per part drops significantly; between five and twenty, it continues to drop but less so. When requesting a quote you can compare up to three quantities: check the curve before deciding how many to order, and if you will need spare parts in a few months, it is usually cost-effective to manufacture them now.
What does not lower the price (even if it seems to)
- Hollowing out the part to save material: every pocket is cutting time; the aluminum left in isn't charged, the aluminum removed is.
- Split a part into two to simplify it: two parts mean two programs, two setups, and one assembly.
- Request a "nice" finish on an internal part: sandblasting or anodizing are charged per batch and add days. When each pays off, in surface finishes for CNC machining.
- Send an STL instead of a STEP: the programmer has to reconstruct the geometry, and that takes time.
How to order to pay a fair price
- Upload a STEP per part.
- Attach a PDF with only the threads and functional dimensions, with their tolerance.
- Explain in one line what the part is for: the engineer can propose a cheaper material or finish that works.
- Request three quantities.
The quote arrives in 24 h with manufacturability review included; if anything in the design increases the part cost without adding function, we will tell you before manufacturing. The design rules for machining on the service page illustrate each point with an example.
Frequently asked questions about CNC machining cost
What is the most expensive factor in machining a part?
Machine time and the number of setups. Small internal radii, deep pockets, tight tolerances across the entire drawing, and machined faces from multiple directions add the most time.
How much does the price per part decrease when ordering more units?
Very significantly between one and five units, because programming and setup time are shared, and more gradually from there. When requesting the quote, you can compare up to three quantities to view the curve.
Is it cheaper to machine aluminum or steel?
Aluminum. It cuts several times faster than carbon steel and three or four times faster than stainless steel. If the prototype can be validated in aluminum, it is the most economical option.
Is there a minimum order for CNC machining?
Yes: the minimum order is 60 € and the minimum manufacturing cost for a machined part is 46 €. Below these figures, no design optimization lowers the price further.