Multi Jet Fusion 3D printing: how it works and when to choose it over SLS and FDM
How an MJF builds layer by layer, what accuracy and materials it offers, and when to choose it over SLS, FDM or machining, with a comparison table.
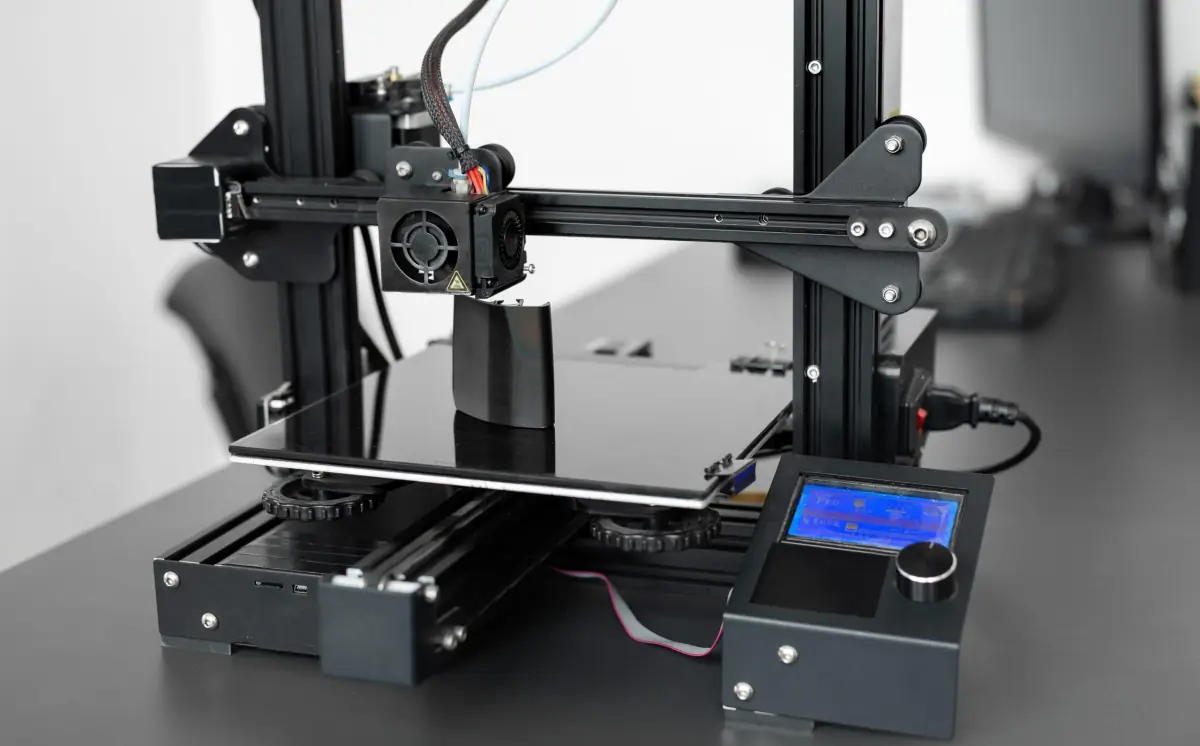
Multi Jet Fusion (MJF) is the 3D printing technology from HP that produces polyamide 12 (PA12) parts by fusing powder layer by layer with ink agents and heat. Parts come out dense, support-free, with a precision of ±0.3 mm up to 100 mm and within a build volume of 380 × 284 × 380 mm. It is the technology we use at Proto&Go! for functional parts: from a single unit and with a lead time of at least 5 working days.
In this guide, we explain how an MJF printer works, what materials and precision it offers, what part size it accommodates, and with a table, when it is advisable compared to SLS, FDM, or machining. If you already have the file, on the industrial MJF 3D printing page for PA12 and TPA, you will find the design rules and how to place your order.
MJF is the option when the part must function: clips, housings, ducts, hinges, tools. Use FDM when the part only needs to exist. Use machining when the material or tolerance is critical. Use vacuum casting when the part needs to look like an injection-molded piece.
How does Multi Jet Fusion 3D printing work?
The process repeats about 1,500 times per build volume, once per 80-micron layer:
- A roller extends a layer of preheated PA12 powder over the platform.
- An injection head, similar to an inkjet printer, deposits two agents: the fusion agent, which is dark, over the part section, and the detail agent on the outline, which cools and defines the edge.
- Infrared lamps scan the layer. Where there is a fusion agent, the powder absorbs the heat and melts; where there is none, it remains loose.
- The platform lowers 80 microns and starts over.
Once finished, the entire build volume cools in a controlled manner for hours: this is what prevents warping and explains why the minimum lead time is in days, not hours. Afterwards, the parts are unpacked: they are removed from the powder block, cleaned with air and shot blasting, and the excess powder is recycled by mixing it with new powder. Since the loose powder supports the part during printing, there are no supports to remove or marks where they were.
MJF vs. SLS and FDM: comparison table
| Criterion | MJF (HP) | SLS (laser) | FDM (filament) |
|---|---|---|---|
| How it melts | Ink + infrared, the whole layer at once | A laser scans the section | Extrusion of melted filament |
| Typical material | PA12, TPA flexible | PA12, PA11, TPU | PLA, ABS, PETG, nylon |
| Layer | 80 µm | 100 a 120 µm | 100 a 300 µm |
| Precision | ±0,3 mm up to 100 mm | ±0,3 mm up to 100 mm | ±0,5 mm or worse |
| Strength | Almost equal in all directions (isotropic) | Almost isotropic | Weak between layers |
| Supports | No | No | Yes, they leave marks |
| Surface | Matte, fine uniform grain | Matte, slightly rougher | Visible layer lines |
| Unit price | Low: the build chamber is filled with many parts | Medium | High per part in short runs |
| Purpose | Functional parts, short runs, assemblies | Similar to MJF | Mockups, initial shape tests |
MJF and SLS compete in the same field and produce similar parts; MJF is faster per build chamber, achieves slightly finer details thanks to the detailing agent, and its parts come out dark gray instead of white. Against desktop FDM, the difference is not in price but in part: an MJF part in PA12 handles loads, clips and threads; an FDM part in PLA doesn't.
What materials are printed in MJF?
PA12, rigid polyamide
It is the default material. Tough, resistant to abrasion and most oils and solvents, with a tensile strength of around 48 MPa and an elongation of 20 %, and stable up to around 80 °C in service. With it, housings, supports, assembly tools, ducts, integrated hinges, and clips that flex thousands of times are made. You have the full datasheet in PA12 for 3D printing MJF.
TPA, the flexible one
A Shore 90A hardness elastomer for bellows, protectors, gaskets, grips, and dampers. Real flexibility depends on both the material and the thickness: a 1.5 mm wall bends, a 10 mm block does not. Its datasheet: TPA flexible for 3D printing.
Colors: PA12 is delivered in natural gray or dyed black; TPA, in natural gray. Neither is transparent: for a transparent part, you must go to vacuum casting or machined polycarbonate.
Precision, tolerances, and part size
- Reference precision: ±0.3 mm on dimensions up to 100 mm and ±0.3 % above; on a 200 mm dimension, ±0.6 mm. If an area must fit with another part, indicate it in the drawing: a fitting hole can be drilled or reamed afterwards.
- Size: the build chamber measures 380 × 284 × 380 mm; we recommend a usable volume of 356 × 280 × 356 mm. Larger parts are studied in sections.
- Walls: 1 to 1.5 mm as a starting point in PA12; more if they are tall or support load.
- Threads: they are printed by modeling the full profile; they work well from M6 and for smaller metric sizes an insert is convenient.
- Texts and logos: letters 2.5 mm high, strokes of 0.5 mm and 1 mm relief as a minimum.
Compare these figures with machining and casting in the manufacturing process tolerances guide.
When to choose MJF and when not to?
Choose MJF for geometries that cannot be machined (internal channels, grids, hollow parts), for assemblies printed all at once, for runs of 1 to several hundred parts without a mold, and for functional prototypes that must withstand assembly and use. The build chamber is filled with dozens of parts, so the price per unit drops significantly in series.
Don't choose it if you need transparency, machining tolerances (IT7), service temperatures above 100 °C, a metal, or a smooth and shiny surface without post-processing. For those cases, CNC machining and vacuum casting are the options; the process selector will guide you in a minute.
Finishes and post-processing
An MJF part comes out dark gray, matte, and with a fine uniform grain, already clean of dust. The usual options are to leave it natural or color it black, which unifies the color and preserves the texture. Other post-processing options (chemical smoothing, painting, hole machining) are studied based on the part; we explain them in 3D printing post-processing.
Price and lead time
The price of an MJF part depends mainly on the material volume and the space it occupies in the build chamber, not on complexity: a hollow part with ribs costs less than a solid block of the same size. That's why hollowing out and lightening is the most direct way to lower the price. You upload the file, choose PA12 or TPA, quantity and finish, and receive the quote in 24 h; parts ship from 5 working days, and the exact lead time for your order is in the quote. If you are unsure whether to print or machine a prototype, read 3D printing: from prototyping to manufacturing.
Frequently asked questions about Multi Jet Fusion
What is Multi Jet Fusion 3D printing?
It is an HP technology that manufactures polyamide parts by fusing powder layer by layer: a head deposits fusing and detailing agents over the powder, and infrared lamps fuse only the section of the part. The parts come out dense, support-free, and with similar strength in all directions.
What precision does an MJF-printed part have?
The reference is ±0.3 mm for dimensions up to 100 mm and ±0.3% above. For a 200 mm dimension, it equates to ±0.6 mm. Areas that must fit with another part are indicated on the drawing and can be machined afterwards.
MJF or SLS: which is better?
They produce very similar parts in PA12. MJF prints the whole layer at once, so it's faster per build and achieves slightly finer detail; its parts are dark gray instead of white. For functional parts in short runs, MJF is usually the most economical option.
How long does it take to print a part in MJF?
At Proto&Go! the quote arrives in 24 h and parts ship from 5 working days. The lead time includes printing, controlled build chamber cooling, cleaning, and finishing, and is set in the quote based on quantity and finish.