Vacuum casting or plastic injection moulding: which to choose?
Investment, lead time, cost per part, materials and tolerances of both processes, and the maths for runs of 50, 300 and 1,000 parts.
For 50 parts, vacuum casting; for 1,000, injection; for 300, it depends on the material and the finish, and that is where it pays off to crunch the numbers. Casting uses silicone molds that yield around 20 copies each and are manufactured in days; injection uses a steel or aluminum mold that costs thousands of euros and takes weeks, but afterwards each part costs pennies and comes out identical.
This guide compares the two processes regarding investment, lead time, cost per part, materials, and tolerances, including the calculation for three series sizes. The casting data refers to our vacuum casting service in silicone molds, which produces runs of 10 to 300 parts in polyurethane starting from 10 working days.
Up to 300 parts, vacuum casting. More than 300 identical parts, injection. Between 100 and 300, or if the design may change, compare the two quotes before ordering the metal mold.
How does each process work?
Vacuum casting
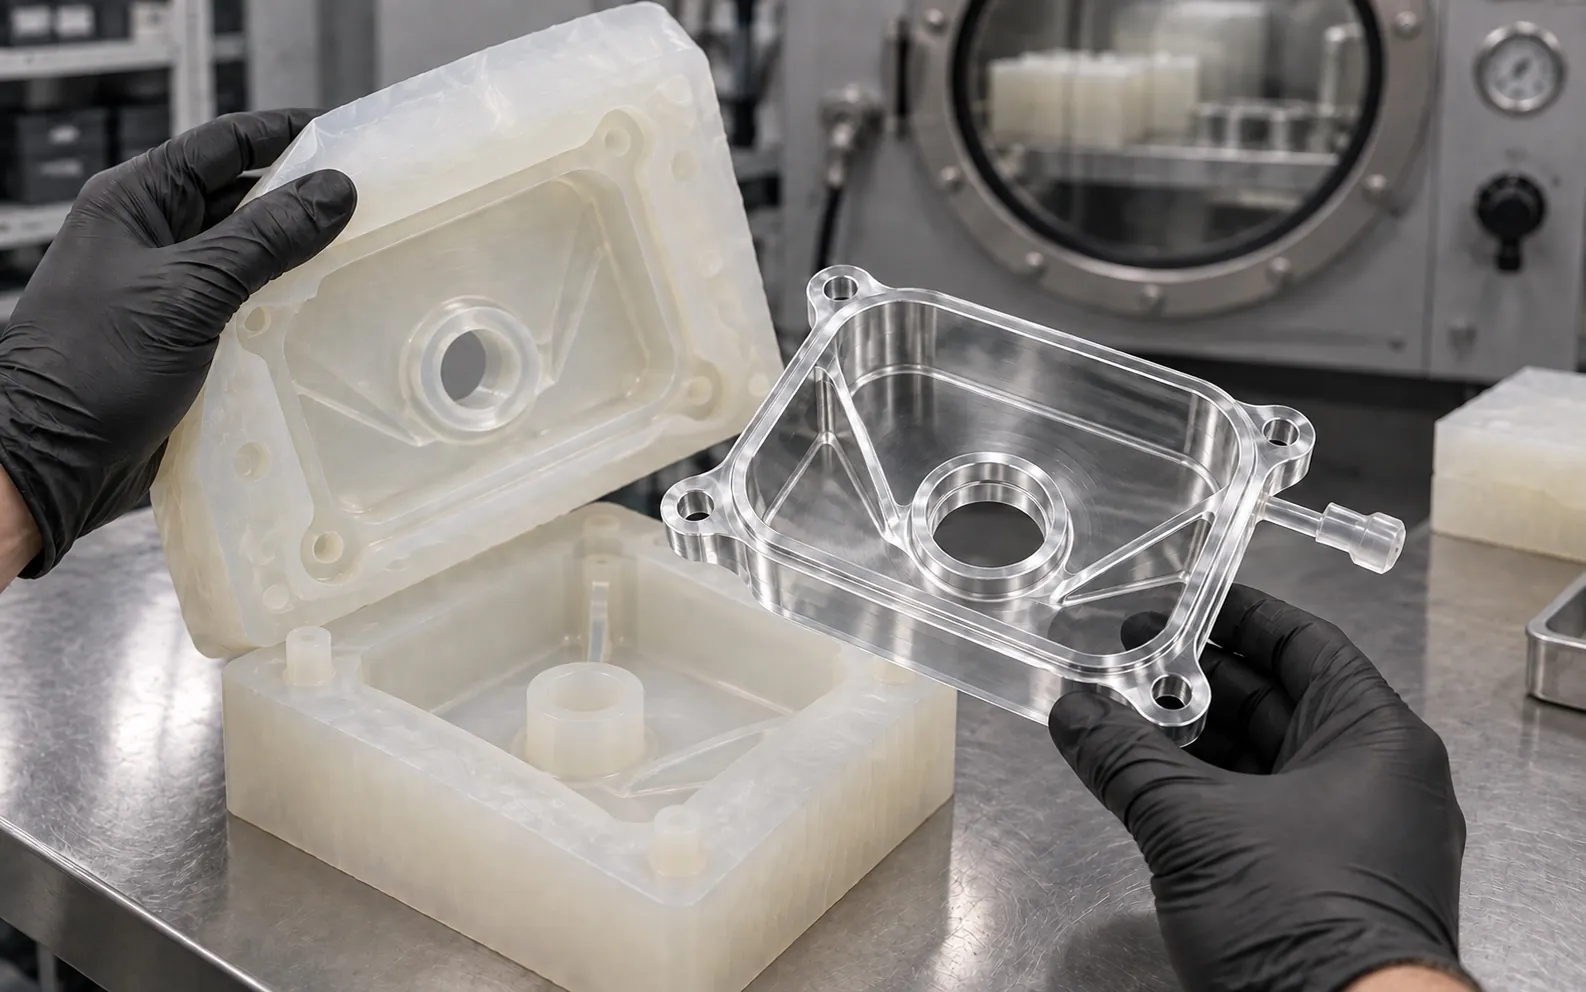
It starts with a master, a machined or 3D printed pattern part finished by hand, which is submerged in liquid silicone. Once the silicone is cured, the block is opened with a scalpel, the master is removed, and the mold remains. Inside, two-component polyurethane is poured into a vacuum chamber, which removes air and prevents bubbles; the part cures in hours and is demolded. A mold lasts around 20 copies before losing definition; for 100 parts, several molds are needed. This is explained step-by-step in silicone molds: process and advantages.
Injection molding
A thermoplastic (ABS, PP, PA, PC…) is melted and injected under pressure into a metal mold that is cooled. The part comes out in seconds, already with its final material. The mold is designed, machined, and adjusted over weeks, and its cost is spread across all the parts that will come out of it, which can be hundreds of thousands.
Comparative table: vacuum casting versus injection
| Criterion | Vacuum casting | Injection molding |
|---|---|---|
| Initial investment | Master and silicone molds: low | Steel or aluminum mold: high |
| First parts | From 10 working days | Several weeks (mold design, machining, and adjustment) |
| Cost per part | Nearly flat: material, labor, and part of the mold | Drops with the series: pennies in long runs |
| Ideal quantity | 10 to 300 parts | More than 300, and especially thousands |
| Materials | Rigid, flexible (30 to 90 Shore A), and transparent polyurethanes that mimic ABS, PC, PMMA, rubber | Real thermoplastics: ABS, PP, PA, PC, POM… |
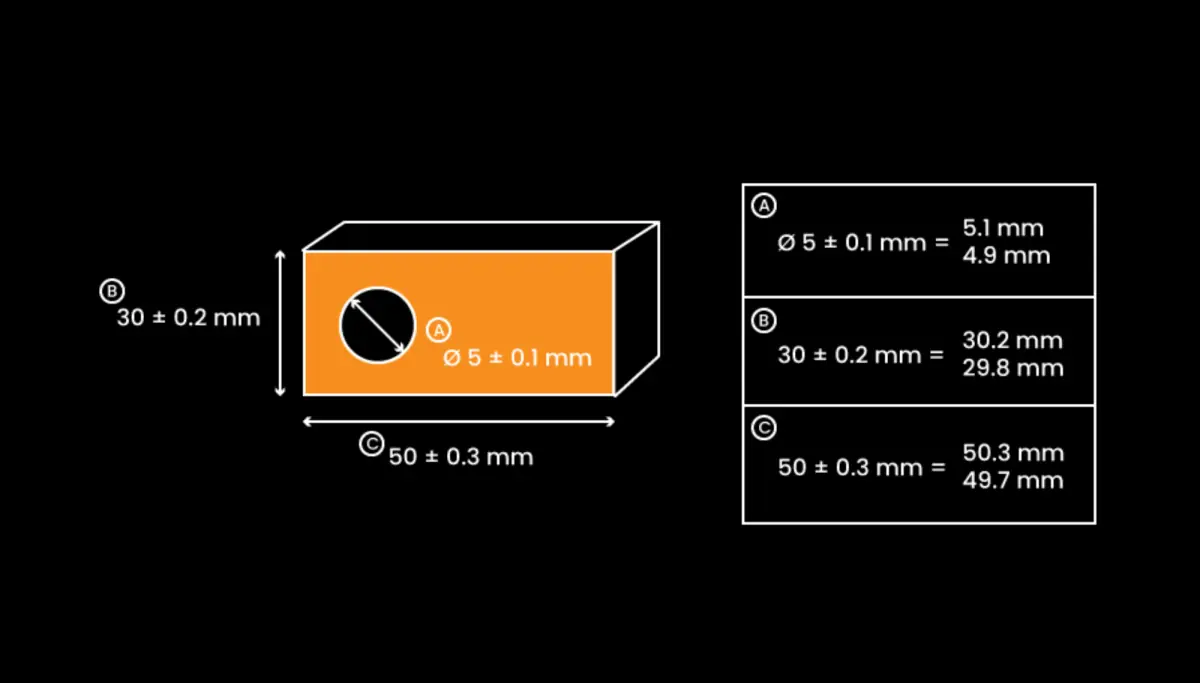
| Tolerances | They depend on resin shrinkage and geometry; they are reviewed during the design phase | Repeatable and tight once the mold is adjusted |
| Finish | The master: gloss, texture, RAL pigmented color in mass or painted | The mold: texture, gloss, color in mass |
| Design changes | One new master and one new mold, in days | Modifying the mold: expensive, sometimes impossible |
| Mold life | About 20 copies | Hundreds of thousands of cycles |
The calculation for 50, 300, and 1,000 parts
The cost structure is different, which is why the answer changes with quantity. In vacuum casting, you pay for the master once, one mold for every 20 parts, and the polyurethane and labor for each casting; the price per part drops slightly by spreading the master cost, but it stays almost flat because another mold is needed every 20 parts. In injection molding, you pay for the mold once, regardless of the run, and each part costs very little.
| Run size | Vacuum casting | Injection molding | What is recommended |
|---|---|---|---|
| 50 parts | 1 master and about 3 molds; parts in 2 or 3 weeks | The mold is amortized over only 50 parts: extremely high unit cost | Vacuum casting, no discussion |
| 300 parts | 1 master and about 15 molds; several casting batches | The mold starts to amortize; the lead time remains in weeks | It depends: vacuum casting if the design can change or the PU material is viable; injection molding if it is the final material |
| 1,000 parts | About 50 molds: too much labor | Amortized mold; identical and cheap parts | Injection molding |
The real crossover point depends on the part size, the finish, and whether the injection mold is aluminum (cheaper, fewer cycles) or steel. That is why we offer casting with up to three quantities: order 50, 100, and 300, and you will see where it stops paying off. If the final run is long, the i-mas team can take the project to injection molding.
The material is not the same: "ABS type" is not ABS
It is the difference most often overlooked. Vacuum casting works with polyurethanes formulated to mimic a thermoplastic: stiffness, color, and touch of ABS, polycarbonate, or rubber. But they are not that material. If you need ABS certification, specific chemical resistance, or PC thermal behavior, you must inject, or machine the real plastic. For housings, covers, visible parts, and validation pre-production runs, polyurethane is more than enough, and it allows something injection molding does not offer in a short run: three hardnesses, transparency, and bulk pigmented color in the same order. The datasheets are in rigid polyurethane and flexible polyurethane.
Tolerances and appearance: what to expect from each
A cast part resembles an injected one, but its precision is not the same: the resin shrinks as it cures and the silicone flexes. Functional dimensions are indicated when requesting the quote and reviewed in the design; a housing that must fit can be machined afterwards. In appearance, casting copies the master with fidelity: gloss, textures, edges, and the color is in bulk (a scratch does not reveal another color) or painted. How to avoid bubbles, sink marks, and parting lines is in how to avoid defects in vacuum casting.
When casting wins even with many parts
- The design is still changing. A pre-production run of 30 units to validate with the client avoids modifying a steel mold.
- Multiple versions of the same part: colors, hardnesses, different logos.
- Large parts or with undercuts that silicone demolds and a metal mold does not.
- Lead time: the first parts in 10 working days versus weeks for the mold.
- Small replacement series every year, without keeping or maintaining a metal mold.
The rules for the part to cast well (uniform thicknesses, angles, undercuts) are in vacuum casting design tips.
How to request the comparison
- Upload the 3D file of the part (STEP preferably).
- Choose the polyurethane (rigid, flexible, or transparent), the RAL or Pantone color, and the finish.
- Indicate up to three quantities, for example 50, 100, and 300.
- Add a PDF if there are inserts, threads, or functional dimensions.
The engineer reviews the design and demolding, proposes where the mold parting goes, and returns the quote in 24 h. We machine the master and make the molds; parts come out in as little as 10 working days. And if the run points to more than 300 pieces, we will let you know before manufacturing.
Frequently asked questions about vacuum casting and injection molding
Vacuum casting or plastic injection for a short run?
For runs of 10 to 300 parts, vacuum casting: silicone molds with low investment, first parts in 10 working days, and final product appearance. For identical runs over 300 parts, injection molding amortizes the metal mold and each part comes out cheaper.
How many parts can be manufactured with a silicone mold?
Approximately 20 copies per mold as a reference. The actual duration depends on the geometry, the resin, and the demolding. For 100 parts, several molds are required, and their number is confirmed upon reviewing the design.
Is vacuum casting polyurethane the same material as injection-molded ABS?
No. It is a polyurethane formulation that mimics the rigidity, color, and feel of ABS, PC, or rubber. It works for housings, covers, and pre-production runs; if you need the certified production material, you must inject or machine the real plastic.
How long does a vacuum casting run take?
The quote arrives in 24 h and the parts are ready from 10 working days. The lead time depends on the quantity, the material, the number of molds, and the finish, and is set in the quote.