Rapid prototyping: what it is and which process to choose at each stage of development
Four stages, four things to validate and the process, material and lead time that suit each one, from the first sketch to the 300-part pre-series.
Rapid prototyping is making a part directly from the 3D model, without molds or tooling, to have it in hand in days and not in weeks. Today it means four processes: 3D printing from 5 working days, CNC machining and sheet metal cutting and bending from 8, and vacuum casting from 10. At each stage of development something different is validated (the shape, the function, the appearance, the run) and that is why the appropriate process changes from one stage to another.
This guide covers the four stages, what is checked in each one and what process, material and quantity is advisable, with the lead times of our service for rapid prototyping and short run manufacturing.
Shape: 3D printing. Function: CNC machining or MJF in PA12. Appearance: vacuum casting. Pre-production run: the production process or the one that most resembles it.
What is rapid prototyping?
The term was born in the 80s with stereolithography: for the first time a part came out of a file without making a mold beforehand. For years "rapid prototyping" was synonymous with 3D printing. Today the concept is broader: any process that makes a custom part from the CAD, without specific tooling, in days. CNC machining, laser cut sheet metal and bent sheet metal, and vacuum casting in silicone molds fit the definition, and each one answers a different question of the development.
The opposite of rapid prototyping is not slowness, but tooling: an injection mold or a stamping die that cost thousands of euros and weeks and that only make sense when the design is no longer going to change.
The four stages and what is validated in each one
| Stage | What is validated | Process | Material | Quantity | First parts |
|---|---|---|---|---|---|
| 1 · Concept | Shape, size, ergonomics | 3D printing | PA12 | 1 a 3 | 5 working days |
| 2 · Functional | Assembly, loads, mechanisms, tolerances | CNC machining or MJF | Aluminum, POM, PA12, TPA | 1 a 10 | 5 to 8 working days. |
| 3 · Appearance | Finish, color, touch, presentation | Vacuum casting or CNC with finish | Polyurethane, anodized aluminum | 1 a 10 | 8 to 10 working days. |
| 4 · Pre-production run | Process, supplier, pilot customer | Vacuum casting, CNC, sheet metal or MJF | The one closest to production | 10 a 300 | 8 to 10 working days. |
Stage 1: the concept prototype
It serves to check that the part fits, is held well, and meshes with the others. It does not need the final material or tolerances: it needs speed and price. MJF 3D printing in PA12 is the default option: no supports, with ±0.3 mm precision up to 100 mm and starting from a single unit. If you only want to see a volume, a desktop printer at home is enough; as soon as the part has clips, threads, or thin walls, PA12 holds up and PLA does not. More about this technology in how 3D Multi Jet Fusion printing works.
Stage 2: the functional prototype
Here the part must work: support load, rotate on a bearing, withstand temperature, or mesh with a purchased part. The process is decided by the material the function needs:
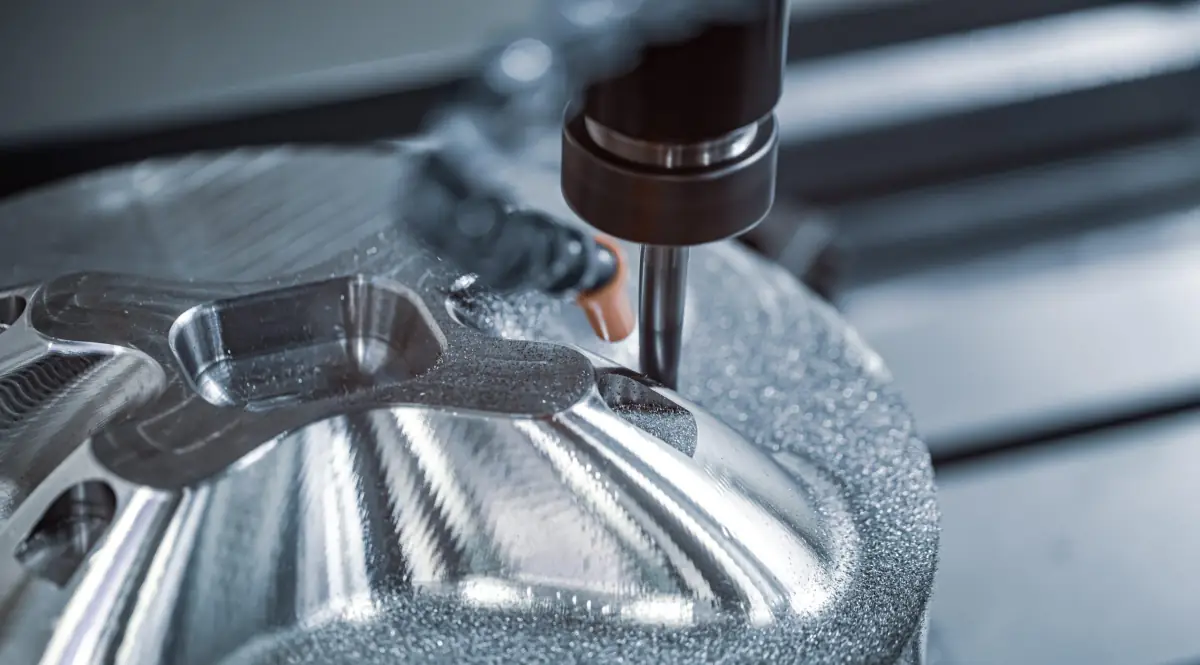
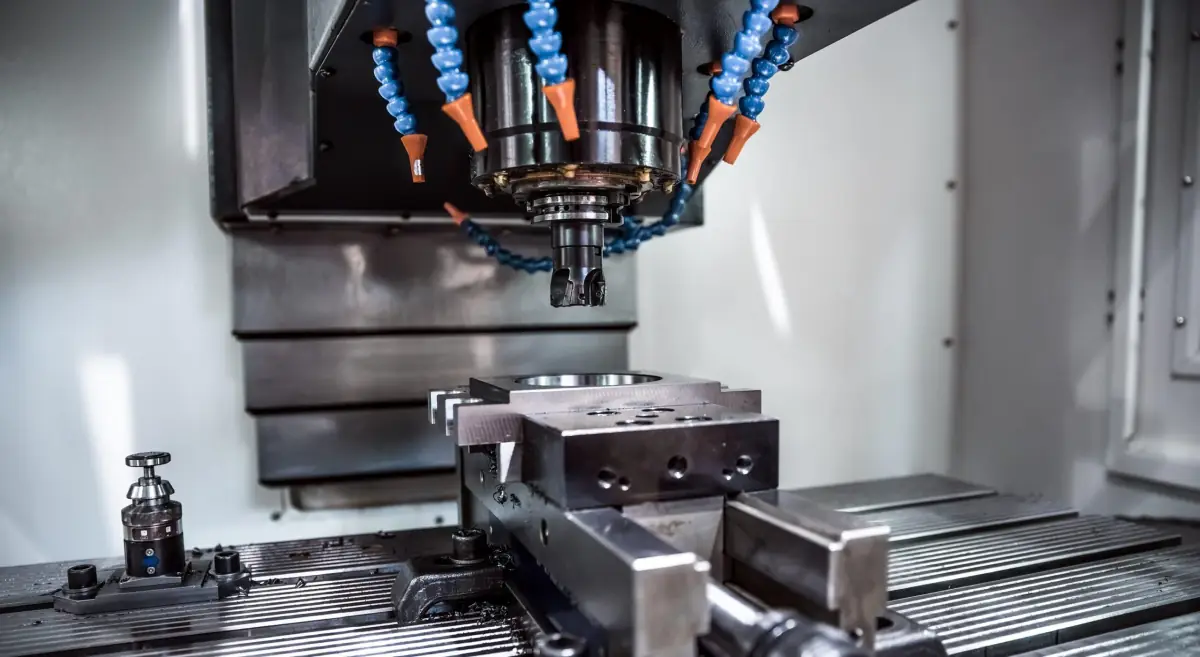
- Metal or engineering plastic with tolerances: custom CNC machining of parts, with general ISO 2768-f tolerance and up to IT7 on fitting dimensions. Aluminum for most cases; steel or stainless steel if there is wear; POM or PEEK for plastic.
- Complex geometry, housings, ducts, clips: MJF in PA12, which withstands assembly and use, and TPA when the part must flex.
- Supports, chassis, and enclosures: laser cutting and sheet metal bending, in steel, stainless steel, or aluminum from 0.3 to 15 mm.
This is the stage where the most is learned and where the most versions are made. A tip: order each version in a single unit and only move to five when the design withstands the test.
Stage 3: the appearance prototype
For a presentation, a trade show, a catalog photo, or a user test, the part must look like the final product: brand color, gloss, texture, transparency. Vacuum casting copies a hand-finished master and produces rigid, flexible, or transparent polyurethane parts in solid RAL pigmented color; it is the closest thing to an injection-molded part without making the mold. For metal, CNC machining with anodizing or painting fulfills the same role. The available finishes are listed in finishes for machined parts.
Stage 4: the pre-production run of 10 to 300 parts
Before ordering an injection mold, it is advisable to put real parts in the hands of pilot customers, build the first units, and validate the process. Vacuum casting is designed for this: about 20 copies per silicone mold, several molds for runs of 100 or 300, and the same appearance on all. If the part is metallic, short run CNC machining lowers the unit price by distributing program and setup; if it is functional in plastic, the MJF build chamber is filled with parts. When each one pays off is explained in vacuum casting or injection: what to choose.
Which process to choose? The decision tree
- Is the part metal or does it need fitting tolerances? → CNC machining.
- Is it sheet metal: flat, bent, with uniform thickness? → Cutting and bending.
- Is it a plastic part with complex geometry, internal holes, or clips, in a run of 1 to 500 units? → 3D printing MJF.
- Does it need to look injection molded, with color and finish, in 10 to 300 units? → vacuum casting.
- More than 300 identical parts with the final material? → Injection molding, and a pre-production run via vacuum casting beforehand.
The manufacturing process selector asks these questions interactively and returns the process and material in a minute. And if the part has two distinct sections, they are combined: housing in PA12 and shaft in aluminum, for example.
How much does it cost and how to lower the price
Without tooling, the first part is the most expensive and from there the unit price drops: in CNC the program and setup are spread across the run, in MJF the build chamber is filled, in casting the master and molds are amortized. Four ways to pay less:
- Request the quote with three quantities and check the curve before deciding.
- Design for the process: 1 mm radii and shallow pockets in CNC machining, 1.5 mm walls and holes with draft angles in MJF, uniform thicknesses and demolding angles in vacuum casting.
- Tolerances only on functional dimensions; general tolerances are already fine. The process tolerances guide explains this.
- Validate on the cheap material what is possible (aluminum before stainless steel, PA12 before painted polyurethane) and reserve the expensive material for the final version.
Five common mistakes
- 3D printing a prototype that must withstand 120 °C or carry a bearing: it is a machined part.
- Ordering ten units of a version that no one has tested.
- Setting ±0.02 tolerances on the entire drawing "just in case".
- Presenting the client with a gray PA12 part when the product will be white and glossy: vacuum casting exists for that.
- Ordering the injection mold before the pre-production run.
Frequently asked questions about rapid prototyping
What is rapid prototyping?
Manufacture a part directly from the 3D model, without molds or tooling, in days. It includes 3D printing, CNC machining, sheet metal cutting and bending, and vacuum casting in silicone molds, depending on what needs to be validated.
Which process is best for a functional prototype?
If the part is metal or requires fit tolerances, choose CNC machining. If it is plastic with complex geometry, clips, or holes, choose MJF 3D printing in PA12. If it is sheet metal, choose laser cutting and bending. Often several processes are combined in the same assembly.
How long does a prototype take?
The quote arrives in 24 hours. The first parts come out in 5 working days for 3D printing, 8 for CNC machining and sheet metal, and 10 for vacuum casting. The specific lead time for each order is detailed in the quote.
How many parts can be made without a mold?
For machining, sheet metal, and 3D printing, from one unit to short runs of hundreds of parts. For vacuum casting, runs of 10 to 300 parts with silicone molds. Above 300 identical parts, injection molding usually compensates.