Surface finishing for CNC machining
Eight finishes, which metal each one suits, how much they thicken or thin the part and how to order them without ruining a thread or a fit.
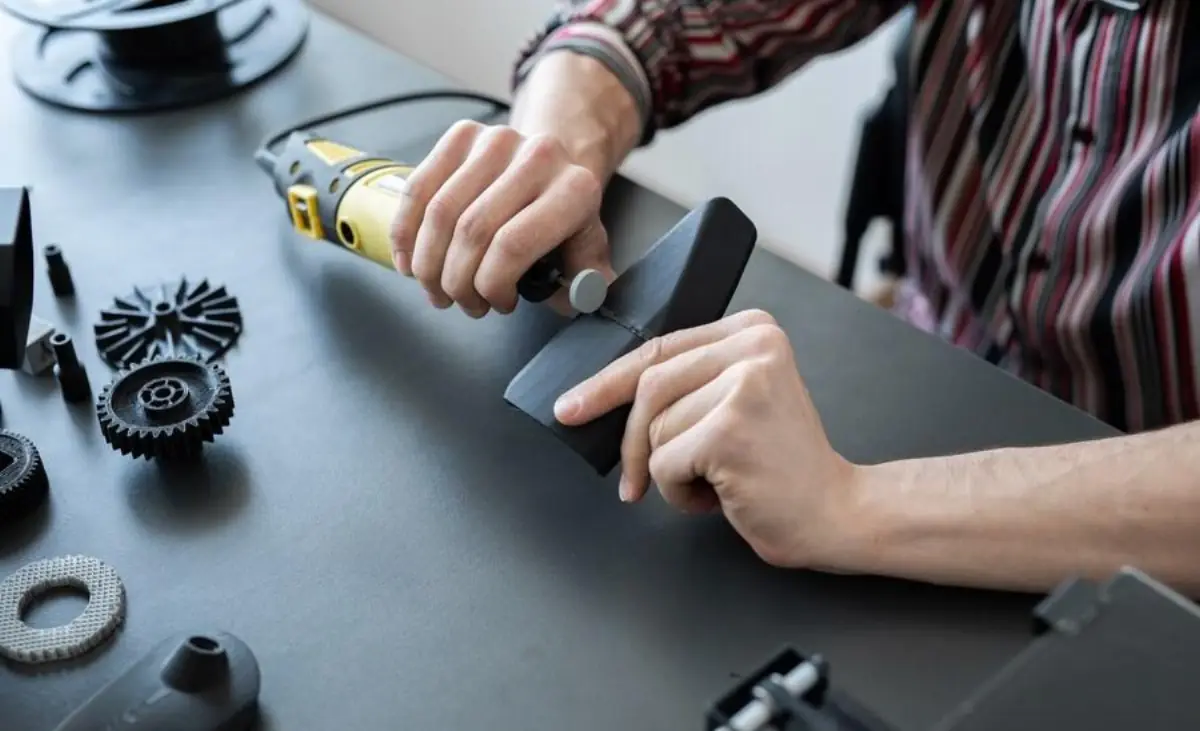
A machined part can be ordered without a finish or with one of eight finishes: anodizing, sandblasting, polishing, bluing, zinc plating, chrome plating, nickel plating, and RAL painting. Four of them change the part dimensions between 2.5 and 100 microns, so it is advisable to decide on the finish before setting tolerances, not after.
In this guide, we explain what each finish adds to custom part CNC machining, which metal it applies to, how much it alters dimensions, and how to order it so that a thread or a bearing housing continues to fit properly. If you prefer to see it in photos, the eight samples from the workshop are on the finishes for machined parts page.
Aluminum that looks good: anodizing. Steel that must withstand: zinc plating or bluing. Visible part in any metal: polishing or RAL painting. Internal or functional part: no finish, which is the cheapest and fastest.
What is a surface finish and what is it for?
When it comes out of the milling machine or the lathe, the part retains the fine marks of the tool: a roughness between 0.8 and 3.2 µm Ra depending on the operation, perfectly valid for most functional parts. The finish is the subsequent operation that changes that surface, and it is done for three reasons:
- Protect. Aluminum and carbon steel oxidize. Anodizing, zinc plating, bluing, and nickel plating form a layer that delays corrosion.
- Give appearance. Sandblasting unifies the tone and erases machining marks; polishing gives shine; paint and anodizing add color.
- Add a function. Hard anodizing and chrome plating harden the surface against wear; nickel plating covers holes and edges uniformly and serves as a base for other coatings.
What no finish does is correct a machining error: a thin wall that vibrated or a radius that was not designed will look the same after anodizing.
The eight finishes: material, thickness, and what each one is for
The table summarizes what we apply to machined parts. Dimensions are indicative and are confirmed in the quote; the sign indicates if the finish adds material (+) or removes it (−).
| Finish | Metals | Dimension change | What it is for |
|---|---|---|---|
| No finish | All | None | Functional or internal parts. The fine marks of the tool remain. |
| Anodizing | Aluminum | +2.5 to 12.5 µm per side | Corrosion and wear protection, available in color. The most ordered in aluminum. |
| Sandblasting | Aluminum, steel, stainless steel, brass | No significant effect | Matte and uniform appearance; hides tool marks. Usually applied before anodizing. |
| Polishing | Stainless steel, brass, aluminum | −5 a 20 µm | Gloss and a smooth surface on visible parts. Removes material: keep it to faces without tolerances. |
| Bluing | Steel | No significant effect | Light black protective layer, without changing dimensions. Typical for tools and equipment. |
| Zinc plating | Steel | +5 a 15 µm | Protection against corrosion with a metallic white-grey appearance. The standard option for steel. |
| Chrome plating | Steel, brass, aluminum | +10 a 30 µm | Surface hardness, gloss, and corrosion resistance. |
| Nickel plating | Steel, aluminum, brass | +5 a 25 µm | Uniform protection also in holes and edges; standard base for other coatings. |
| RAL painting | Metal and plastic | +40 a 100 µm | Color to choice according to RAL chart, in matte, satin, or gloss. It is the thickest layer. |
Which finish to choose according to the material?
Aluminum
The machined aluminum is anodized. It is an electrochemical process that converts the surface itself into aluminum oxide: it is not a glued layer, so it does not flake. It admits color (black, natural, red, blue...) and, if sandblasted beforehand, the result is matte and uniform. If you want to know more, you have an article on how machined aluminum is anodized.
Carbon steel
It oxidizes in weeks if left bare. For general use, zinc plating; for tools, guides, and machine parts where the dimension cannot change, bluing; for wear or shine, chrome or nickel plating.
Stainless steel
It does not need protection. It is requested without finish, sandblasted for a uniform matte, or polished when the part is visible or needs to be cleaned well (feeding, laboratory).
Brass and copper
Polishing for decorative parts or electrical contact; nickel plating when brass needs to be prevented from darkening over time.
Engineering plastics
POM, nylon, or polycarbonate are delivered without finish or painted. Polishing is possible in polycarbonate and acrylic when transparency is sought.
How does the finish affect tolerances and threads?
It is the question that prevents the most problems. A conventional anodizing forms a layer of 5 to 25 µm that grows more or less half outwards and half inwards into the metal: each face gains between 2.5 and 12.5 µm and a diameter, double. A shaft thickens and a drilled hole narrows. Hard anodizing forms layers of 25 to 75 µm and changes dimensions much more.
Our general tolerance, if you do not specify anything, is ISO 2768-f, which is ±0.1 mm on a 25 mm dimension, so the finish fits within most parts. The issue arises with fits: an H7 housing of 25 mm has a total tolerance of 21 µm, and anodizing can consume the entire margin. There are three ways to resolve this:
- Machine with the corrected dimension: the hole is machined a few microns larger and then anodized to measure. This is what we do by default when the drawing indicates the fit.
- Mask: the fit area or the thread is covered and remains uncoated. This is indicated in the PDF drawing.
- Thread afterwards: on painted parts, the thread is re-tapped after the finish.
With RAL paint, there is no doubt: 40 to 100 µm do not fit in any thread or fit, so threads and bearing surfaces are always masked. If your part has fits, calculate the margin with the ISO 286 tolerance calculator and read the guide on machined part tolerances.
How much does a finish add to the lead time and price?
Machining comes out of the workshop from 8 working days. Most finishes are done by specialized companies in the area and add several days, which are already included in the quote date. Sandblasting and bluing are the fastest; colored anodizing, chrome plating, and RAL paint are the ones that take the longest.
Regarding price, the finish is charged per batch and not per piece, so its relative weight drops significantly in a short run: anodizing one part costs proportionally more than anodizing twenty. And the combination of sandblasting + anodizing, which is the one that looks best on visible aluminum, consists of two operations and two prices.
How to order the finish without surprises
- Upload the STEP to the platform, choose the material, and select the finish in the part dropdown.
- If it is paint or colored anodizing, indicate the RAL reference or the color in the comments field. The image on the screen is for reference.
- Mark on a PDF the threads, fits, and bearing surfaces that must remain uncoated.
- If a dimension must be met after the finish, state it in the drawing: the engineer will correct the machining dimension.
- For a visible part, request a sample unit before the run. It is cheaper than repeating twenty.
Any doubt regarding compatibility is resolved by the engineer who reviews each order: if you request chrome plating on aluminum or anodizing on steel, they will propose the alternative that works before manufacturing.
Frequently asked questions about finishes in CNC machining
Which finish is the most economical for an aluminum part?
No finish. If the part is visible, sandblasting is the next most economical and hides tool marks. Anodizing adds protection and color and is the most requested for visible aluminum.
Does anodizing change part dimensions?
Yes, slightly. Each face gains between 2.5 and 12.5 microns and a diameter, double that. It does not matter for a part with general tolerances; for an H7 fit, indicate it on the drawing to machine with the corrected dimension or mask the area.
Can steel be anodized or aluminum be chrome plated?
Anodizing is only for aluminum. Steel is protected with zinc plating, bluing, chrome plating, or nickel plating. Aluminum does admit chrome plating and nickel plating, although anodizing is usually the better option for price and adhesion.
What happens to threads when a part is painted?
RAL paint adds between 40 and 100 microns and blocks any thread, so threads and bearing surfaces are masked before painting. Indicate them on the PDF drawing when requesting a quote.
Can I request a specific RAL or Pantone color?
Yes. Indicate the reference and the gloss level (matte, satin, or glossy) in the order. The final tone has a small tolerance and a screen image does not validate the color: for branded parts, request a sample.