The different machining tools: types and when each one is used
Five families of tools, what they are made of and how the diameter of an end mill decides the radii, depths and price of your part.
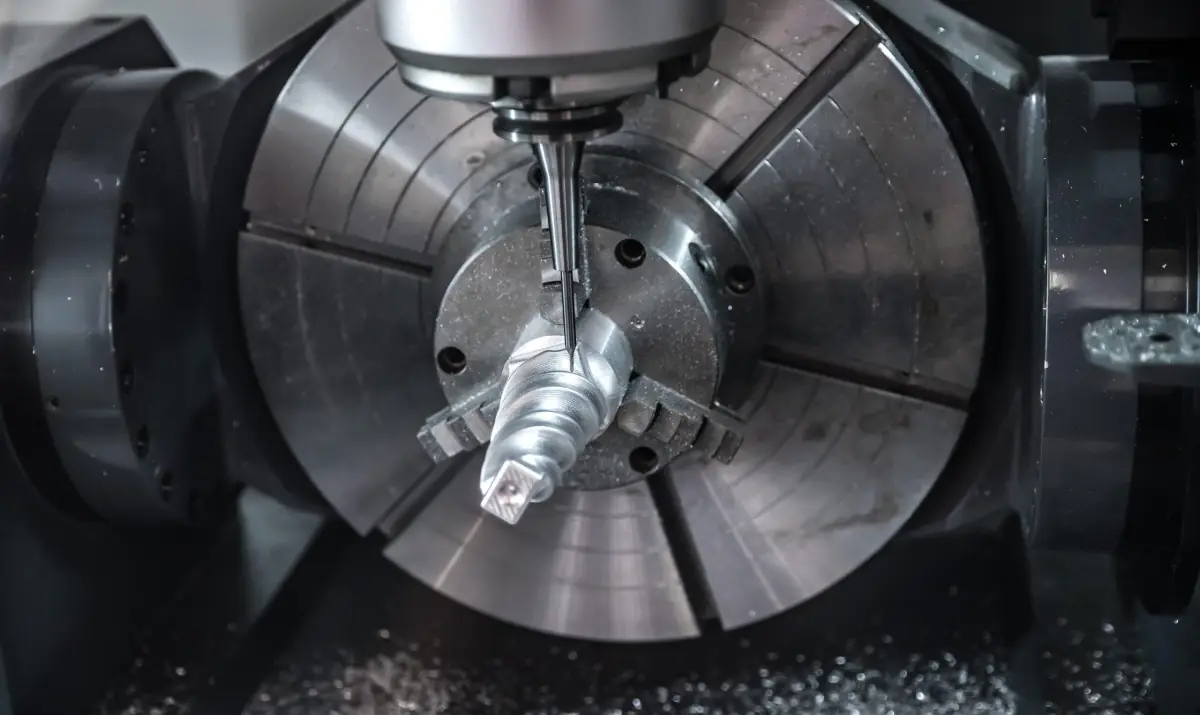
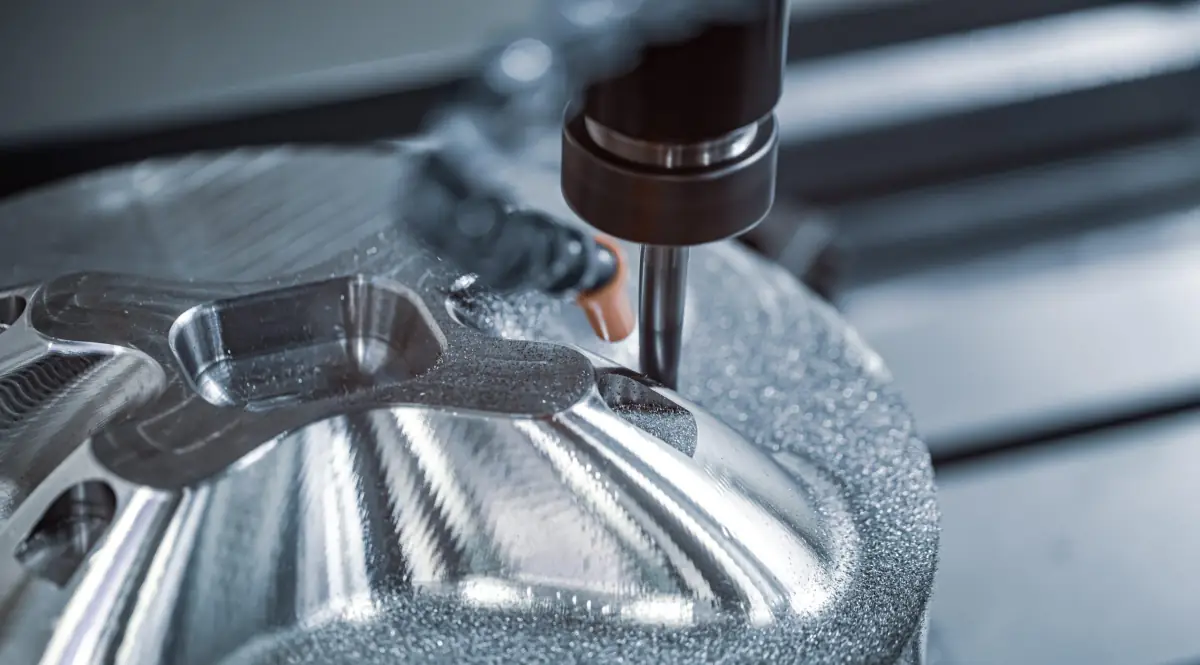
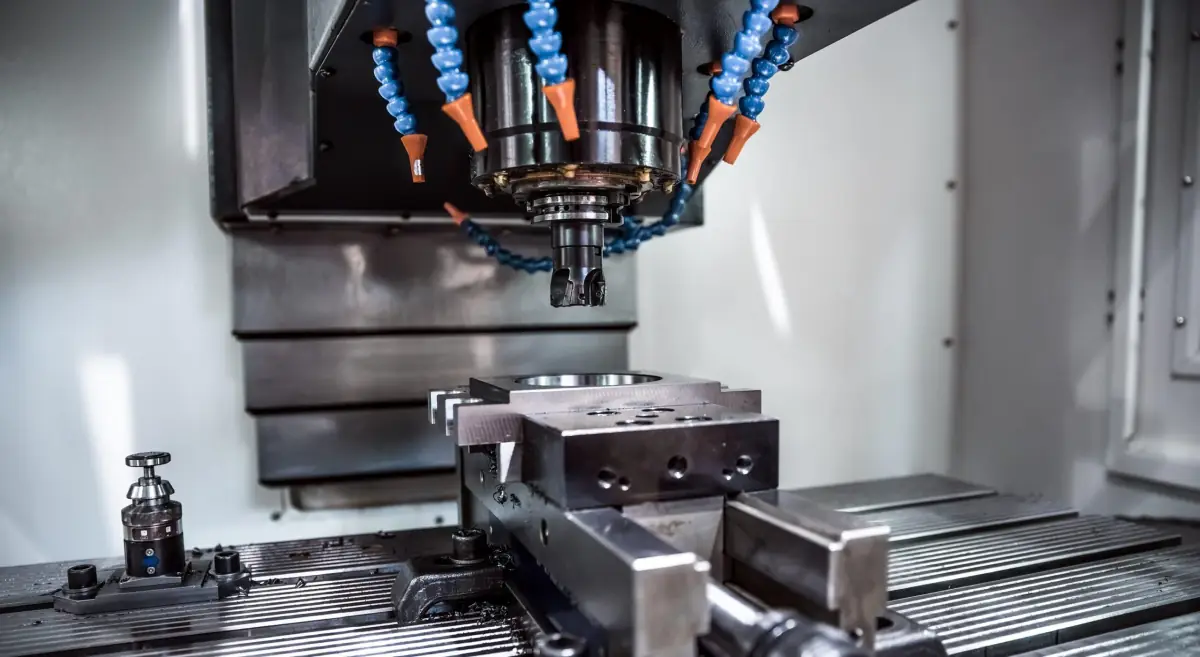
Machining tools are grouped into five families: end mills, drills, reamers, threading tools, and turning inserts. A standard part goes through three or four of them: it's roughed out with a carbide end mill, drilled, threaded, and finished with a smaller end mill. And the tool that most conditions your design is the end mill: its diameter sets the minimum internal radius and how far a pocket can go.
This guide explains what each tool does in CNC machining of custom parts, what material they're made of, why they wear out, and, above all, how to design the part so it can be machined with large, rigid, and fast tools, which is what lowers the price.
It's not the machine, it's your geometry: the radius of internal corners, pocket depths, and drill diameters dictate what tool is needed, and that tool dictates machine time.
What types of tools are used in CNC machining?
End mills
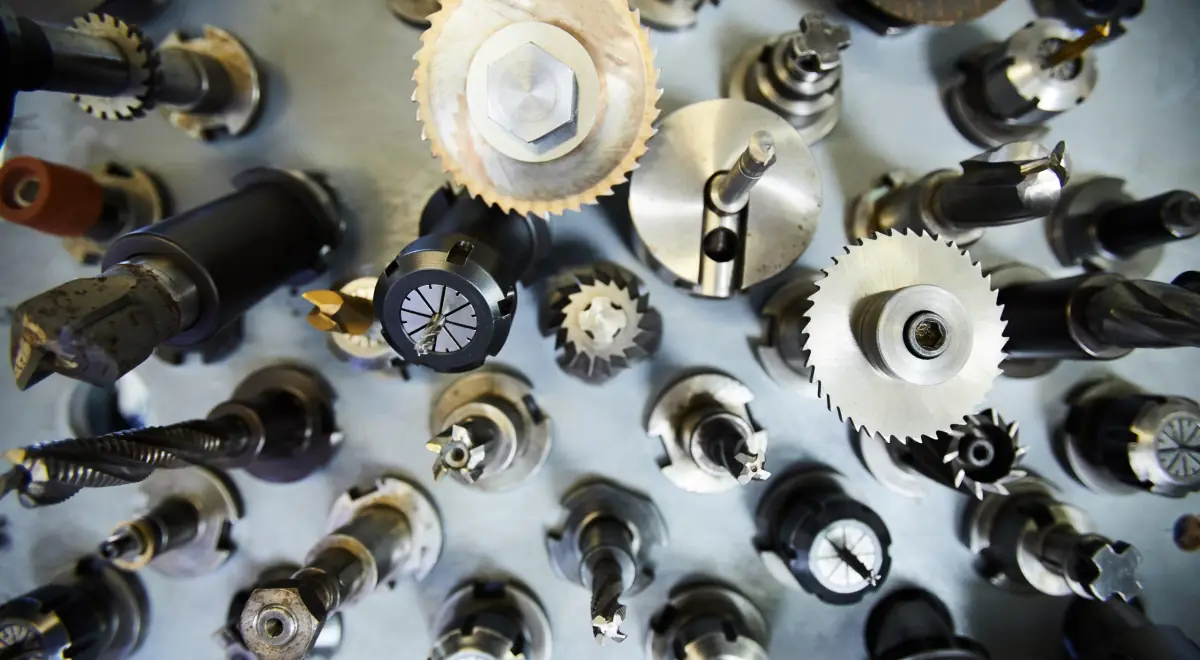
They are rotating tools with multiple flutes that remove material as they advance over the part. The most common ones in a machining center:
- Flat end mill or slot drill: cylindrical, with 2, 3, or 4 flutes. It cuts contours, pockets, and slots. It's the default working tool.
- Ball end mill: spherical tip for curved surfaces, molds, and 3D finishes.
- Bull-nose end mill: cylindrical with rounded corners. Sturdier than a flat end mill for roughing, and it leaves radii at the bottom of the pocket.
- Face mill: large diameter with interchangeable inserts. It flattens large faces in few passes.
- Chamfer mills and disc cutters: for breaking edges and for deep, narrow slots.
Drills
They make drilled holes. In CNC, carbide drills with internal coolant are used for holes up to 4 or 5 times their diameter in depth; beyond that, a long drill and chip evacuation cycles are needed, which increase time.
Reamers
They rework an already drilled hole to leave it with the exact size and good surface finish. It's the tool used to achieve an H7 housing for a bearing or pin.
Threading taps and threading mills
The tap cuts the thread in one axial pass; the threading mill generates it via interpolation and works for various metrics with a single tool. In hard materials or large threads, the threading mill is safer because it doesn't get stuck.
Turning inserts
In the lathe, the tool does not rotate: it is a carbide insert held in a tool holder. There are inserts for turning, facing, grooving, threading, and boring, and each has a nose radius (0.2 to 1.2 mm) that leaves the same radius on diameter changes of the part.
Table: which tool performs each operation and which mark appears on your design
| Tool | Operation | What is machined on your part |
|---|---|---|
| Flat end mill | Contours, pockets, grooves | Internal radius = radius of the cutter. Design radii of at least 1 mm and one-third of the pocket depth. |
| Ball end mill | Curved surfaces | The smaller the detail, the more passes and more time. Avoid bottom radii smaller than 0.5 mm. |
| Slab mill | Large flat faces | Flat faces are cost-effective. A small protrusion in the middle of a face forces a switch to a smaller cutter. |
| Drill | Drilled holes | Depth up to 4 × diameter in blind holes. Prefer standard diameters (3, 4, 5, 6, 8, 10 mm). |
| Reamer | Precision holes | Only where there is a fit (H7). Each reamed hole is a separate tool and an additional operation. |
| Tap or threading cutter | Threads | From M3, useful length of 3 × diameter and unthreaded margin at the bottom. The metric is in the PDF. |
| Turning insert | Bore, face, and groove | Radius at diameter changes of 0.2 to 1.2 mm. Narrow and deep grooves require special tooling. |
What material are the machining tools made of?
The tool material must be significantly harder than the part and withstand cutting temperatures. From least to most performance:
- High-speed steel (HSS): economical and tough. Used in drills and taps for aluminum and plastics, and in conventional machines.
- Hard metal (tungsten carbide): the standard tool in CNC. Cuts at two to three times the speed of HSS and maintains the edge on steel, stainless steel, and titanium.
- Cermet: between hard metal and ceramic. For fine finishes on steel.
- CBN and polycrystalline diamond (PCD): the former for hardened steels and the latter for high-silicon aluminum, composites, and graphite. Expensive, but last dozens of times longer.
Almost all hard metal tools have a coating of a few microns (golden TiN, violet TiAlN, grey AlCrN) that reduces friction and extends life. For aluminum, uncoated or specifically coated end mills are used, because aluminum sticks to some coatings.
How does the tool affect the price and finish of your part?
The price of a machined part is mainly machine time. And time is dictated by the smallest tool required by your design:
- A 10 mm end mill removes material several times faster than a 3 mm one and does not vibrate. Every internal corner with a 1 mm radius in a 30 mm deep pocket requires finishing with a 2 mm end mill, slow and fragile.
- A wall under 0.8 mm in metal or 1.5 mm in plastic vibrates during cutting, deforms, and leaves a poor finish, no matter how well the tool is sharpened.
- Each distinct hole type (metric, diameter, tolerance) is an additional tool in the changer and an extra operation.
- A tighter tolerance than the general one (ISO 2768-f in metal) requires slow finishing passes and more measurement. Reserve fine tolerances for dimensions that need them, as explained in the guide to tolerances in machined parts.
Surface finish also comes from the tool: a new end mill and a light pass leave a smooth surface; a worn tool leaves it matte and with burrs. That is why the workshop controls the life of each edge and, for visible parts, finishes with a fresh tool. If you seek another appearance, check surface finishes for CNC machining.
Why do they wear out and how are they controlled?
Each cutting edge has a tool life measured in minutes of cutting, depending on the material, speed, and cooling. CNC shops manage this with three mechanisms: tool life counters in the numerical control, which alert when to change the tool; presetting, which measures the actual length and diameter of the tool before mounting so the program compensates for wear; and in-machine measurement with a probe, which checks the part without unclamping it. This is what allows machining unit 20 just like unit 1, and what makes a well-prepared CAM program produce repeatable parts, as we explain in the article about CAM software in CNC machining.
Six rules for designing with the tool in mind
- Internal radii of at least 1 mm, and larger the deeper the pocket (one-third of the depth is a good reference).
- Pockets shallower than 3 or 4 times their width. If you need more, split the part or open the pocket from another side.
- Through-drills whenever possible; blind holes up to 4 times the diameter, in standardized diameters.
- Threads from M3, with 3 diameters of useful length, and indicated in the PDF: the 3D model does not specify the metric.
- Walls of 0.8 mm or more in metal and 1.5 mm in plastic.
- Fewer types of holes and different radii: each one is an additional tool. The design rules for machining on the service page illustrate them one by one.
If you are unsure whether to machine the part on a lathe or a mill, which also changes the tools and the price, read CNC lathe and CNC mill: differences.
Frequently asked questions about machining tools
What tool leaves a radius on the inner corners of a part?
The end mill. As it rotates, it cannot leave a sharp inner corner: it leaves a radius equal to its own. Design radii of at least 1 mm so a rigid end mill can be used, and if another part with sharp corners must fit there, add a bend relief on the corners.
Do I have to specify which tools are used on my part?
No. The engineer reviewing the order and the CAM programmer choose the tools based on the geometry and material. You only specify material, quantity, finish, and, in a PDF, the threads and dimensions with tolerance.
Why does a small and deep drilled hole increase the part cost?
A thin drill going deeper than 4 or 5 diameters has to retract several times to clear the chips and feeds slowly so it doesn't break. A through hole, or a shallower one, takes a fraction of the time.
Do carbide tools work for plastics?
Yes, and they are the usual ones. For plastics and aluminum, carbide end mills with very sharp cutting edges are used, and often without coating, because these materials tend to stick to the tool.